Which Screen Media Survives Wet Coal Screening?
Nov 2, 2026
 admin
Quick Answer
Neither material wins everywhere. Rubber liners outlast steel in wet, fine grinding with balls up to roughly 80 mm, weigh about a sixth as much, install faster and run quieter. Steel wins where impact dominates: SAG and AG mills, large media, hot or dry grinding. Composite liners with alloy lifter bars serve the large wet ball mills in between. Decide with a wear audit, a pulp temperature reading and a real ball top size, then compare cost per tonne ground.
What Is a Rubber Mill Liner vs Steel Mill Liner?
They are the two standard wear surfaces inside a tumbling grinding mill. Rubber liners are moulded plate and lifter segments, elastic and light, fixed with T-bolts and sealing washers. Steel liners are castings, manganese or alloy steel, heavy and impact resistant. Which one is better depends entirely on media size, pulp temperature and the impact energy of the duty.
Key Takeaways
Summary Table
| Item | Description |
| Function | Protect the mill shell, lift the charge and set the charge motion profile that controls grinding |
| Material | Rubber (natural/SBR compounds), alloy or manganese steels, or composites with steel lifters in a rubber body |
| Application | Wet secondary and regrind ball mills for rubber; SAG, AG, rod and hot dry mills for steel |
| Service life | Duty dependent; wear rate in mm per 1,000 hours measured on site is the only honest figure |
| Benefits | Rubber: longer life in fine wet duty, lighter plates, lower noise, no iron contamination. Steel: impact strength, heat tolerance |
Definition
Mill liners are the replaceable wear surface inside a tumbling **Grinding** mill. Every **Grinding Mills** installation asks the same three things of its **Mill Liners**: shield the shell from the charge, lift the media and pulp so mill power becomes breakage, and set the charge motion profile.
Rubber liners are moulded from natural or SBR rubber compounds, typically 40-70 Shore A, in plate and lifter segments fixed with T-bolts and sealing washers. Steel liners are castings, manganese steel, chrome-moly alloy or high-chrome irons, bolted through countersunk holes. Composite liners combine the two, an alloy steel lifter bar carrying impact at the leading edge with a rubber body carrying abrasion behind it. On a **Ball Mill** the same definitions apply at every size, from a small regrind unit to a multi-megawatt production machine.
Working Principle
A mill liner works by shaping how the charge moves. At normal operating speed the lifters carry media and pulp up the shell wall until the charge either cascades down its own surface or cataracts, launching clear of the toe. Cascading grinds by abrasion. Cataracting adds impact breakage.
The liner’s job is to keep that motion in the designed band as the liners wear. A fresh profile grips the charge and lifts it high. A worn profile lets the charge slip, power draw falls, and the mill grinds less while consuming the same electricity. Watch the power draw trend between relines and you’re watching liner condition through the only instrument that never lies.
Cast steel and moulded rubber hold their profiles differently through a campaign. Steel keeps its lifting face long, then loses it fast near end of life, and the power draw drops visibly in the last weeks. Rubber changes shape gradually, which keeps charge motion steadier for more of the campaign. Steady motion means steady grind, and some plants notice the mill running more consistently on rubber before anyone counts the wear measurements.
Wear mechanisms differ by material. On steel, abrasive particles plough grooves and impact deforms the surface; work-hardening grades such as Hadfield manganese build surface hardness under the beating. On rubber, a particle pressing into an elastic surface displaces material instead of cutting it, and the rebound returns part of each impact to the charge. Rubber fails on heat, on cutting from tramp metal or oversize media, and on installation faults.
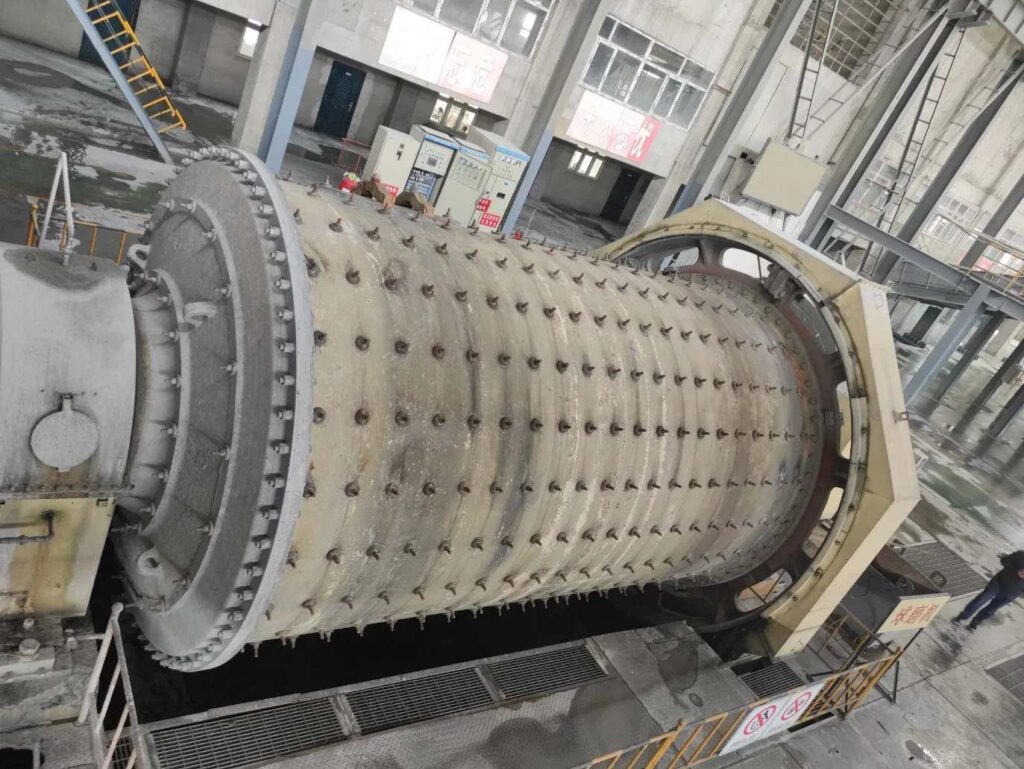
Ball mill shell lined with bolted liner plates during a relining shutdown
A ball mill shell during relining. Bolt pattern, segmentation and door size are the details a supplier needs before quoting either material.
Benefits
Rubber’s benefits concentrate in wet fine grinding. Longer wear life against fine abrasive slurries. Roughly a sixth of the steel weight, which shortens relines and allows plate handling through the manhole on mid-size mills. Two fitters with a trolley can do work that once took a crane crew and a rigging plan. Markedly lower noise, sometimes enough to change the hearing-protection zoning in the mill building. Almost no metal contamination of the pulp, which matters where downstream **Flotation** chemistry is sensitive to iron.
Steel’s benefits concentrate in impact and heat. It carries large media and coarse feed without tearing. It tolerates hot or dry grinding that would age rubber in weeks. It holds decent scrap value at replacement. Composite designs such as **Ball Mill Liners & Heavy-Duty Mill Lining Systems** add a middle path: alloy bars absorbing impact with rubber carrying the abrasive body wear, often the cheapest choice per tonne ground on large wet ball mills near the 80 mm boundary.
Applications
Rubber liners suit wet secondary ball mills, regrind mills and fine grinding duties where media top size stays below about 80 mm and pulp temperature stays within the compound’s rating. Steel liners suit SAG and AG mills, rod mills, primary ball mills with large media, and any dry or hot grinding application. Composite designs suit the boundary zone: large wet ball mills running 70-90 mm balls, where neither pure material is clearly right.
Duty matching starts with the circuit around the mill. Coarse feed from upstream **Crushing** keeps sharp edges longer and cuts rubber harder. Fines from a retop-sized **Classification** stage shift wear in rubber’s favour. The **Grinding Media** charge is the load the liner must survive, so its top size belongs in the first supplier conversation. And a mill fed by **Grinding Rods** is a different wear problem altogether, since rod line contact chews profiles that balls merely scuff.
Material Comparison
| Property | Rubber liner | Steel liner | Composite |
| Density | About 1.1-1.2 g/cm³ | About 7.8 g/cm³ | Between, by design |
| Weight per set | Roughly one sixth of steel | Baseline | Between |
| Best wear mode | Fine wet abrasion | Impact plus abrasion | Mixed duty |
| Temperature tolerance | Most compounds rated below roughly 70 °C continuous | Handles hot pulp and dry grinding | Follows the rubber used |
| Media top size | Commonly rated to about 80 mm balls | No practical limit from the liner side | Extends rubber’s range upward |
| Noise | Markedly lower | Baseline | Lower than steel |
| Installation risk | High; over-torque cuts rubber, missing washers leak | Moderate; errors appear later as cracks | Moderate |
| End-of-life mode | Tearing and chunking, sometimes sudden | Thinning then break-through, usually caught at inspection | Lifter bar wear visible early |
Two mills with the same nameplate can wear liners at very different rates, so conditions at your plant decide the purchase. Treat the table as a screening tool. Treat your own wear audit as the decision.
Application Comparison
Compare the two materials the way a metallurgist would, duty by duty.
Wet secondary ball mill, 40-80 mm balls, fine abrasive feed: rubber usually outlasts steel, and the lighter set pays back the change-out every reline. SAG or AG mill with large rock and balls: steel, because the impact energy per event is beyond what rubber compounds tolerate, which is exactly the work **SAG Mill Liners** are cast for. Rod mill: steel, for the line-contact reason above. Dry or hot grinding: steel again, because rubber’s temperature rating is a hard ceiling and a marketing claim doesn’t move it. Corrosive slurry: rubber or composite, since corrosion that thins steel plate doesn’t touch elastic materials.
The regrind case deserves its own note. In a fine regrind mill the wear is nearly pure abrasion at low impact, rubber’s strongest mode and steel’s weakest. Plants that switch such a duty from steel to rubber very often find the new set outlasts the old one. That’s also the cheapest experiment in liner selection: one section of the shell, one campaign, measured honestly.
Industry Application Matrix
| Industry | Typical duty | Recommended liner |
| Gold, wet secondary ball mill | 50-80 mm balls, abrasive slurry | Rubber or composite |
| Copper, SAG mill | Large rock and balls, high impact | Cast steel or alloy |
| Iron ore, fine regrind | Small media, heavy abrasion | Rubber |
| Coal, dry grinding or hot feed | Heat plus abrasion | Steel |
| Lead-zinc, corrosive slurry | Acidity plus fine grinding | Rubber or composite |
| Lithium, fine grinding circuit | Small media, temperature control | Rubber |
| Cement, hot clinker grinding | Heat, dry, large charge | Steel |
| Phosphate, wet attrition | Fine wet abrasion | Rubber or composite |
Selection Guide
Four numbers select the material, and all four are cheap to get right.
Media top size first, because impact energy grows roughly with the cube of ball diameter and rubber’s margin shrinks fast past about 80 mm. Check the actual **Grinding Balls** recharge size rather than the design sheet. Pulp temperature second, measured at discharge, against the compound’s written continuous rating. Critical speed third, since higher speed lifts the charge harder. Feed size fourth, from the preparation stage ahead of the mill.
Then run the boundary check. Below 80 mm, wet, cool pulp: rubber, with composite as insurance on large mills. Above it, hot or dry: steel. In between: price both plus a composite option as cost per tonne ground.
One more selector people forget. What does the downstream circuit tolerate? Iron released by steel liners reports to the next stage, and if the next stage is a sensitive separation process, rubber’s clean wear counts double. Ask the metallurgist before the purchase order, since the mill’s cheapest option can be the circuit’s expensive one.
Procurement Guide
The quote is only as good as the data behind it. Send a supplier this set and you’ll get comparable numbers back.
| Item | Why the supplier needs it |
| Mill diameter and effective grinding length | Sets plate size and segmentation |
| Existing liner drawings or OEM part numbers | Allows replacement manufacture to the original geometry |
| Mill type and discharge arrangement | Overflow, grate and pulp lifter designs differ |
| Media type, top size and charge volume | Governs impact load and material choice |
| Percent critical speed | Governs charge motion and profile design |
| Feed size and product size (F80, P80) | Sets the abrasion versus impact balance |
| Pulp temperature and pH | Screens rubber compatibility |
| Operating hours per year | Converts life into a calendar schedule |
| Photos and thickness readings of worn liners | Turns a claim into a diagnosis |
Ask every candidate supplier the same questions. Can you manufacture to our drawings? Can you provide material and compound certificates? Can you support OEM replacement part numbers? Will you state the compound’s temperature rating in writing? A supplier who quotes from diameter and length alone is selling weight, not a solution.
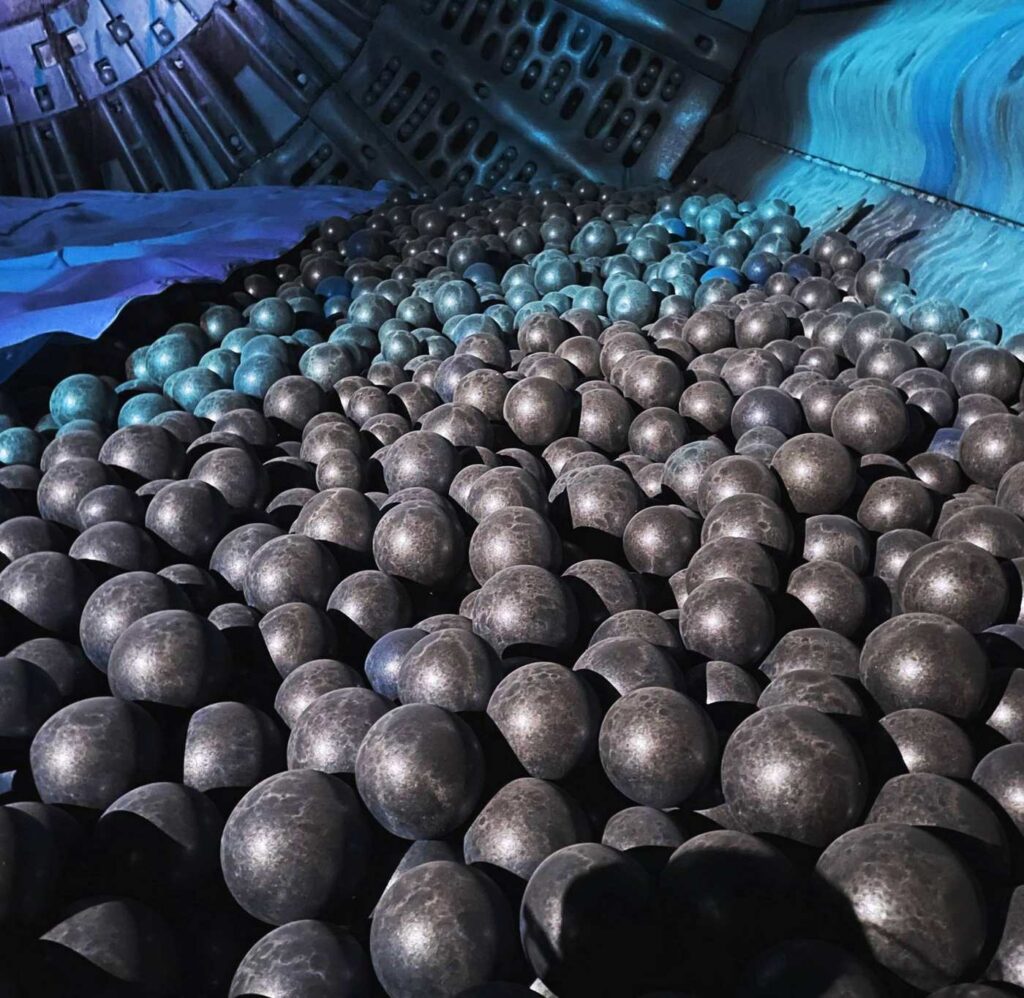
Inspector checking liner and grate wear inside a large grinding mill
Wear inspection inside a large mill. Measured thickness at fixed reference points turns reline timing into arithmetic.
Failure Analysis
| Problem | Possible cause | Recommended solution |
| Rubber torn at lifter leading edge | Oversize media, tramp metal, or profile worn past its limit | Screen for tramp, review media top size, check the compound’s impact rating |
| Rubber cracked and brittle | Pulp temperature above the compound’s rating | Measure discharge temperature, request a heat-resistant grade, or move to steel |
| Steel plate cracking at bolt holes | Over-torque, misaligned seating, or vibration | Verify torque pattern, re-seat plates, inspect hole quality |
| Uneven wear around the shell | Charge slipping, profile mismatch, poor feed distribution | Check power draw trend, review feed size and distributor settings |
| Slurry weeping at bolt holes | Missing sealing washer or under-torque on rubber | Re-torque with correct washers at the first inspection |
| Power draw falling over weeks | Worn lifter profile letting the charge slip | Bring the reline forward; a slipping charge grinds less and wears the shell |
| Premature composite failure | Lifter bars worn before the rubber body | Review media top size and attack angle with the supplier |
Maintenance Guide
Installation quality decides whether either material reaches design life. Steel plates go in shell first, ends last, torqued to the manufacturer’s pattern and seated hard against their neighbours; a 10 mm gap breaks the leading plate early. Rubber adds two requirements: sealing washers under every bolt head, and torque discipline, because over-tightening cuts rubber while under-tightening lets it pump.
Run a re-torque pass after the first run-in period on both materials. Plates bed in and joints close. Then inspect on a rhythm. Daily, listen for metallic impact sounds and check the discharge for shell leaks. Weekly, walk the mill and look for slurry weeping at bolt lines. Every scheduled shutdown, measure thickness at the marked reference points and log millimetres per thousand hours against the previous reading.
A wear rate that suddenly doubles at one segment is telling you something specific, a profile mismatch, a media change or a feed shift. Catch it at inspection and it’s a plate order. Miss it and it’s a shell repair with the plant watching. Spare parts policy belongs in the same conversation: a set of critical plates on the rack costs less than one unplanned extension of a shutdown.
Case Study
Customer type: mid-size gold operation, wet grinding circuit.
Ore type: free-milling gold ore, moderately abrasive.
Operating conditions: secondary ball mill, 60 mm ball top size, wet slurry at ambient temperature, continuous operation.
Problem: the plant was replacing cast steel shell liners on a short cycle, and every reline consumed a full crane crew across a long shutdown. Between relines, power draw drifted down as profiles wore and the charge began to slip.
Solution: a wear audit showed media top size and pulp temperature sitting well inside rubber’s envelope, so the shell was converted to moulded rubber liners with composite plates at the high-impact feed end, made to the existing geometry.
Result: on the plant’s own measurements, the rubber set’s wear rate came in below the steel rate for this fine wet duty, the power draw held steadier through the campaign, and the lighter plates cut the change-out crew and crane time. A representative outcome for this duty class; confirm your own numbers with an audit.
FAQ
Can rubber mill liners handle large grinding balls?
Only up to a point. Suppliers commonly treat roughly 80 mm ball top size as the practical limit for rubber, because impact energy climbs steeply with ball diameter. Above that, rubber tears and chunks at the lifter leading edge. For bigger media, use composite liners with alloy lifter bars or move to steel.
How long do rubber liners last compared with steel?
No single number is honest without duty data. In wet fine grinding with small media, rubber commonly outlasts steel, and the gap widens as the duty gets finer and wetter. In high-impact or hot duty, steel wins by a wide margin. Measure both wear rates in your own mill, then compare cost per tonne ground.
Are rubber liners suitable for SAG mills?
Generally no, not as the primary shell liner. SAG duty combines large rocks, large balls and high impact energy, the combination rubber tolerates worst. Some plants run rubber or composite components at the discharge end where impact moderates. For the shell, cast steel or alloy liners remain the standard choice.
What temperature can rubber mill liners take?
Most standard compounds are rated for continuous pulp temperatures below roughly 70 °C, and heat-resistant grades extend that somewhat. The rating varies by compound, so ask for the number in writing, then measure the actual pulp temperature at the mill discharge rather than trusting the design sheet.
Why are my steel liner plates cracking at the bolt holes?
Usually torque or seating. Over-torqued bolts stress the hole, misaligned plates carry load unevenly, and vibration finishes the crack. Verify the torque pattern, re-seat the plates hard against their neighbours, and inspect hole quality. Cracking along one row of bolts points at that row’s seating.
Can I mix rubber and steel liners in one mill?
Yes, and mills do it deliberately. Steel or composite plates take the high-impact feed end while rubber carries the fine-grinding zones toward discharge. Match plate geometry at every joint so the charge can’t catch a step, and record which sections wear fastest so the next set corrects the balance.
What information does a liner supplier need to quote?
Mill dimensions, existing liner drawings or OEM part numbers, media top size and charge volume, critical speed, feed and product sizes, pulp temperature and pH, plus photos and thickness readings of the worn liners. With that set, a supplier can quote to your geometry and put a defensible life expectation behind the price.
Is the noise reduction from rubber liners significant?
Yes, and it’s a compliance issue as much as a comfort one. Rubber-lined mills run markedly quieter than steel-lined ones, often enough to change hearing-protection zoning in the mill building. The exact reduction depends on mill size and speed, so measure it at your own site.
Conclusion
Rubber wins wet, fine and abrasive. Steel wins big, hot and violent. Composite splits the middle on large ball mills near the boundary. Choose with four measurements, media top size, pulp temperature, critical speed and feed size, then price every option as cost per tonne ground including downtime. Buy from a supplier who manufactures to your drawings and states the compound’s rating in writing. The mill tells the truth at every shutdown, so write the numbers down.
Related Articles
Related Products
Related Technical Guides
Related Buyer Guides
Related Comparison Articles
Contact
Annie Lu
Email: annie.lu@huataogroup.com
WhatsApp/WeChat: +86 18032422676
Website: www.tufflexscreen.com
admin