How Long Does a Flotation Rotor Last? An Engineer’s Guide to Wear, Measurement and Replacement
-
 admin
- 17 Nov, 2026
Quick Answer: A flotation rotor lasts from months to over a year depending on ore abrasiveness, slurry chemistry, speed and the stator it works against; supplier references list 10-15 months for some polyurethane rotors and 3-8 for rubber, indicative only. The useful number comes from blade thickness measured at fixed points against the OEM limit, divided by the site’s own monthly wear rate. Replace on that forecast, inspect the stator at every rotor change, and trial any material change in one cell first.
What Is Flotation Rotor Service Life?
The flotation rotor, or impeller, is the component that turns electrical power into flotation: suspension of particles, dispersion of air, circulation through the stator. Its service life is the interval before blade wear degrades that hydrodynamics past the process’s tolerance. Wear changes geometry, geometry is function, and function is metallurgy. A worn rotor announces itself as weaker circulation and drifting recovery before it ever fails structurally, which is why rotor life belongs in the process conversation as much as the maintenance one.
Life varies enormously between sites, and the variation is honest: it reflects the ore, the chemistry, the speed and the maintenance discipline. The plants with the longest intervals are usually the ones measuring, not the ones lucky.
Key Takeaways
✔ Blade thickness at fixed points, divided by monthly wear, is the replacement schedule.
✔ The rotor-stator pair is one hydrodynamic machine; inspect it as one.
✔ Speed changes move wear, power and metallurgy together; trial them together.
✔ Polyurethane versus rubber is a duty decision decided by a one-cell trial.
✔ Annualised cost including downtime beats purchase price in every comparison.
Summary Table
| Item | Description |
| Function | Maintain suspension, circulation and air dispersion |
| Key metric | Blade thickness vs OEM limit, per month of wear |
| Factors | Ore abrasiveness, slurry chemistry, speed, stator condition |
| Material options | Polyurethane and rubber compounds |
| Outcome | Planned replacement and stable metallurgy |
Definition
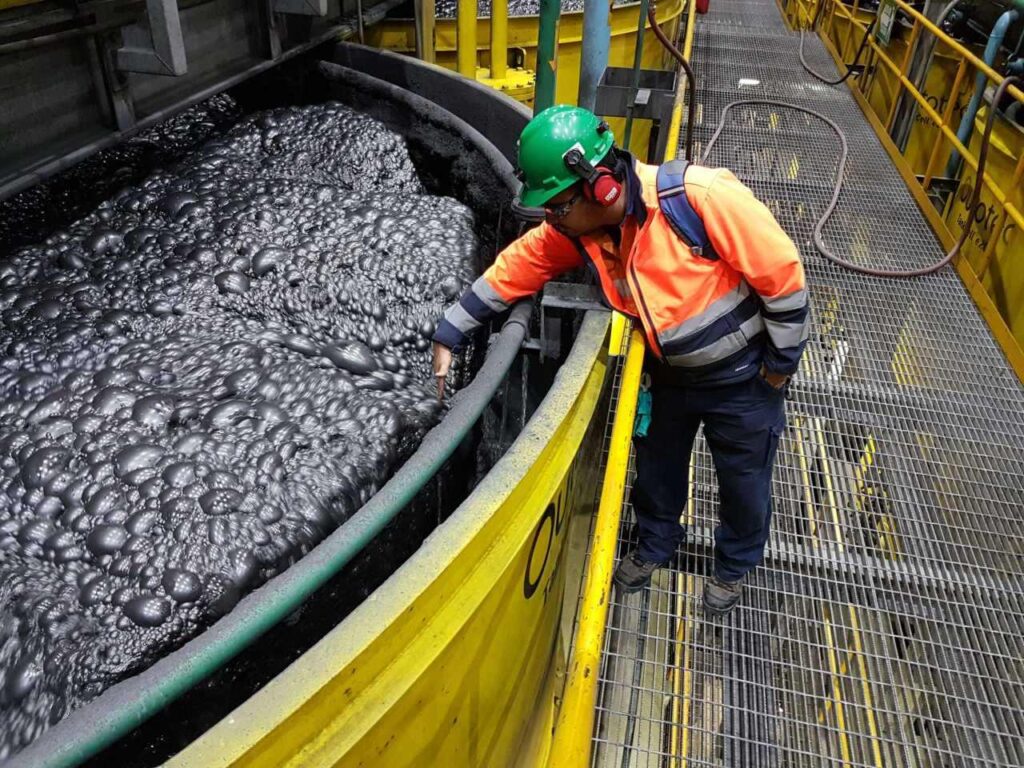
Flotation rotor blade geometry
The blades are process equipment; their wear is process drift.
Flotation rotor service life is the operating interval before blade wear degrades pumping, air dispersion or circulation beyond the process’s tolerance, or before wear reaches the manufacturer’s structural limit. It is set by four interacting factors and measured by one simple routine. The rotor works as half of a coordinated assembly with the stator, and both halves wear.
Working Principle
Four factors set the wear rate, and each is measurable.
Ore abrasiveness leads. Hard angular particles in quartz-rich copper and gold feeds grind elastomer surfaces on contact; coarser distributions add localised impacts; and any change in ore source, grinding performance or upstream classification moves the wear rate even when the cell is untouched.
Slurry and chemistry set the material’s environment. Solids concentration drives contact frequency; reagents, pH and temperature decide whether a compound holds, swells or softens. A formulation proven in one circuit can deteriorate in another, which is why compatibility is verified, and never assumed.
Speed sets the relative velocity between particles and blade. Higher tip speed increases abrasive loading, but reducing speed blindly risks suspension and recovery. The published Cannington FloatForce trial cut speed 10%, reported 17% power savings and improved wear and recovery, on that mechanism, with their measurements. The lesson is the method: changes go through controlled trials, not opinions.
The stator completes the hydrodynamic pair. Metso’s CFD research ties rotor wear to reduced pumping and power intake, and stator wear to weakened turbulence and altered flow. Evaluating the rotor alone misreads half the machine.
Measurement converts all four factors into a schedule. Blade thickness at consistent points, every shutdown, logged against months. Remaining thickness over the monthly wear rate gives remaining life: a 30 mm blade at 24 mm with an 18 mm limit and 1 mm per month of wear has six months of planning room. The estimate is linear and for planning only; accelerated wear moves the date earlier, never later.
Benefits
- Replacement enters planned shutdowns instead of emergency response.
- Metallurgy stays stable because blade geometry stays within specification.
- Annualised parts cost falls as measured life extends.
- Spare-parts stocking becomes forecastable.
- Warranty and supplier discussions gain a factual basis.
Applications
Rotor wear concentrates in abrasive circuits: quartz-rich copper and gold concentrators, silica-laden industrial minerals, and any plant where upstream screening lets foreign objects through to the cell. Published ranges are wide, from six-month cycles to fifteen months after mechanism upgrades, and the width is the point: every site owns its number.
Foreign-object damage deserves a paragraph of its own, because it masquerades as abrasion and corrupts every wear forecast built on it. Oversized rocks and broken metal chew blades locally, obstruct air and slurry passages, and produce damage patterns that uniform slurry wear never does. The defence lives upstream: screen and classification efficiency, vibration investigated when it appears, passages checked at planned shutdowns. When blade damage concentrates in a small area, the question is the cause before the replacement; a new rotor installed into the same mechanical fault repeats the failure at the same price. Localised wear is a diagnosis, not a destiny.
Material Comparison
| Selection factor | Polyurethane | Rubber |
| Abrasive slurry | Often suitable with an appropriate compound | Depends strongly on rubber formulation |
| Impact and flexibility | Grade-dependent | Can offer high resilience |
| Chemical compatibility | Must verify reagent, pH and temperature | Must verify rubber compound compatibility |
| Dimensional stability | Formulation-dependent | Formulation-dependent |
| Maintenance planning | Use measured wear rates | Use measured wear rates |
Application Comparison
| Situation | Wrong response | Right response |
| Recovery drifts between shutdowns | Add reagent | Measure blades and clearances first |
| Rotor fails before the forecast | Blame the supplier | Check foreign objects and speed changes |
| Stator worn with the rotor | Replace rotor only | Coordinate replacement or justify retention |
| New material considered | Convert the whole circuit | One-cell trial with wear measurements |
| Speed raised to fix suspension | Accept the wear | Trial speed against metallurgy and wear |
Industry Application Matrix
| Industry | Typical duty | First consideration |
| Copper | Abrasive quartz feed | Polyurethane compound evaluation |
| Gold | Coarse abrasive particles | Speed and foreign-object control |
| Coal | Moderate fines | Rubber resilience options |
| Industrial minerals | Variable chemistry | Chemical compatibility first |
| Potash / salts | Crystalline abrasion | Formulation trials |
Selection Guide
- Record the current state: hours, blade measurements, wear photographs.
- Establish the wear rate from at least two measurement cycles.
- Verify cell model, mounting and stator compatibility before quoting.
- Match material to the dominant mechanism: abrasion, impact or chemistry.
- Trial any material change in one representative cell.
- Replace on the forecast, inspecting the stator at every rotor change.
Procurement Guide
Buy against wear data. The enquiry package carries the cell manufacturer and model, original part numbers, drawings or samples, required material, ore type, particle size, slurry density, pH, reagent environment, operating speed and current rotor life. Test each supplier on three questions: which compound for our ore and chemistry, and why; what dimensional tolerances and mounting interfaces you guarantee; will you support a one-cell trial with measurements at defined intervals. Relevant detail is in the rotor and stator wear parts guide and the rotor-stator overview. Suppliers who quote from drawings are engineering; suppliers who quote from a material name are guessing.
Failure Analysis
| Problem | Possible Cause | Recommended Solution |
| Recovery drifts between shutdowns | Blade wear changing geometry | Measure and forecast replacement |
| Exposed metal on blades | Elastomer worn through | Immediate replacement assessment |
| Abnormal vibration | Imbalance or drive problems | Investigate the complete assembly |
| Poor air dispersion | Rotor, stator or air-system issue | Inspect the complete mechanism |
| Localised blade damage | Foreign object or misalignment | Find the cause before replacing |
| Rapid wear after material change | Chemical or duty mismatch | Trial again with compatibility verified |
Maintenance Guide
Every shift, review vibration, motor load, air flow and unusual changes. Weekly, trend operating data and investigate deviations. Planned shutdowns: inspect blades and stator vanes, measure thickness at repeatable points, check clearances and fasteners, remove foreign material. Periodically, update the remaining-life forecast. Every replacement: document wear patterns, hours and reasons. Cell entry follows isolation, lockout, drainage and confined-space procedures without exception.
Case Study
Customer Type: Copper concentrator, abrasive quartz-bearing ore.
Operating Conditions: Continuous flotation circuit, rotor replaced approximately every six months.
Problem: Unplanned rotor failures and recovery drift between replacement cycles.
Solution: Blade thickness measured at fixed points every shutdown; wear rate established; polyurethane impeller trial in one representative cell; stator inspected at every rotor change.
Result: Replacement moved to a measured forecast, unplanned failures stopped, and the trial data supported a compound decision backed by the site’s own wear records.
FAQ
- How often should flotation rotors be replaced in a copper mine?
On measured blade wear against the OEM limit, not on a calendar. Site intervals range widely; Nui Phao’s six-to-fifteen-month improvement came from a mechanism upgrade.
- What happens if a rotor is not replaced in time?
Pumping and air dispersion weaken, recovery drifts, and if the elastomer wears through, slurry attacks the metal structure with costlier consequences.
- Can a polyurethane rotor replace a rubber rotor?
When dimensions, properties, mounting and operating characteristics are compatible, yes, with chemistry verified and a one-cell trial before circuit-wide adoption.
- Does rotor speed affect service life?
Yes, through relative particle velocity and abrasive loading. Speed changes belong in controlled trials weighing wear, power and metallurgy together.
- Should rotor and stator be replaced together?
Not automatically. Replace on each component’s measured condition; coordinate only where both approach their limits in the same shutdown.
- How is remaining rotor life estimated?
Current blade thickness minus the OEM minimum, divided by the monthly wear rate from repeated measurements.
- What causes localised blade damage?
Foreign objects, misalignment or mechanical faults rather than uniform abrasion. Diagnose before installing the replacement.
- What data should we send for a quotation?
Cell model, part numbers, drawings or samples, material requirements, ore and slurry details, operating speed and current rotor life.
- How do we compare polyurethane and rubber honestly?
Equivalent geometry, similar conditions, documented wear measurements, ideally as a one-cell trial. Supplier figures are indicative, never controlled comparisons.
Conclusion
Flotation rotor life is a measurement looking for a habit. The blades carry the schedule in their thickness, the stator shares the geometry, and the process announces wear before the structure fails. Measure the wear rate, replace on the forecast, inspect the pair together, and buy materials on documented trial data. Plants that do this stop replacing rotors on rumour and start replacing them on arithmetic, and their flotation circuits hold their metallurgy between shutdowns instead of drifting toward them.
Related Articles
Related Products
- Flotation Spares (Rotor & Stator)
- Flotation Impeller & Stator
- Flotation Rotor & Stator Parts
- Flotation Cells
- XCF/KYF Flotation Cell
Related Technical Guides
- Flotation Cell Rotor and Stator Wear Parts
- Rotor & Stator in Mechanical Flotation Cells
- Hydrocyclone Wear: Root Causes, High-Wear Zones & Material Solutions
- Hydrocyclone Underflow Too Wet? 6 Causes & Fixes
- Improve Fine Screening Efficiency with Polyurethane Screen Panels
Related Buyer Guides
Related Comparison Articles
Contact
Annie Lu
Email: annie.lu@huataogroup.com
WhatsApp/WeChat: +86 18032422676
Website: www.tufflexscreen.com
Tags:
 admin
personal profile