How Often Should I Replace Hydrocyclone Liners?
Oct 20, 2026
 admin
Applications
Flotation wear parts are used in mechanical flotation cells across copper, lead-zinc, nickel, gold, phosphate and rare earth processing. The most critical components are generally those that experience severe wear, require frequent replacement or create significant operational consequences when they fail.
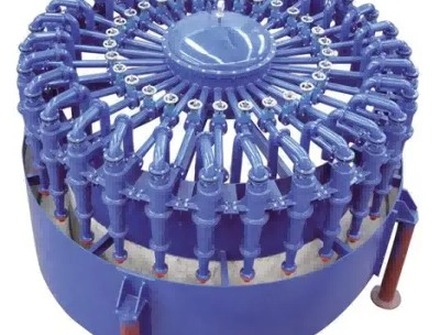
Rotors and stators are usually the first components to examine when maintenance costs are high. Impellers and related flotation components may also experience substantial wear, particularly in applications involving hard minerals, high solids concentrations or demanding operating conditions. For upstream process context, see Hydrocyclones, which often feed flotation circuits after classification.
Material Comparison: Rubber vs. Polyurethane
| Evaluation factor | Rubber | Polyurethane |
|---|---|---|
| Abrasion resistance | Depends on compound | Often advantageous in abrasive applications |
| Impact resistance | Generally very good | Depends on formulation and hardness |
| Dimensional stability | Depends on compound and conditions | Often a key advantage |
| Chemical compatibility | Must be verified | Must be verified |
| Initial purchase price | Varies by design and supplier | Varies by grade and manufacturing process |
| Potential ROI advantage | Impact resistance and application suitability | Longer useful life under suitable abrasive conditions |
There is no single material that provides the best ROI in every flotation application. Rubber and polyurethane (PU) are both widely used. Their suitability depends on slurry abrasiveness, particle size, impact loading, chemical exposure, temperature and equipment design.
Polyurethane is often selected for its abrasion resistance and dimensional stability. In applications where continuous abrasion is the main failure mechanism, a properly formulated PU rotor or stator may maintain its working profile longer than a conventional rubber alternative. However, polyurethane performance depends on formulation, hardness, curing quality, component geometry and chemical compatibility. A product described simply as “PU” does not guarantee a particular service life.
Rubber offers flexibility and good impact resistance. It can be an effective option where coarse particles or repeated mechanical impacts are important wear mechanisms. A well-designed rubber component may provide excellent lifecycle value when its material properties match the application. For related wear-material guidance, see Hydrocyclone Wear: Root Causes, High-Wear Zones & Material Solutions.
Application Comparison: When Each Material Wins
Polyurethane may improve ROI when abrasive wear is dominant. If the original rotor failed mainly because of severe impact, however, switching materials without addressing the impact mechanism may not solve the problem.
A practical trial, supported by wear measurements and operating records, can provide stronger evidence than a general material claim.
Industry Application Matrix
| Industry | Typical Flotation Wear Challenge | Recommended Focus |
|---|---|---|
| Copper Ore | Abrasive slurry, high tonnage | Polyurethane rotor/stator, wear monitoring |
| Lead Zinc Ore | Chemical exposure, fine particles | Material compatibility verification |
| Gold Ore | Variable feed, impact loading | Rubber or composite where impact dominates |
| Nickel Ore | Hard minerals, high solids | Dimensional stability and clearance control |
| Phosphate | Slurry chemistry, abrasion | Chemical compatibility and wear rate data |
| Rare Earth | Fine particles, process stability | Rotor-stator geometry and performance tracking |
Selection Guide
A useful starting point is to review maintenance records and identify components with the highest combination of:
Replacement frequency
Direct purchase cost
Installation labor
Downtime consequences
Potential impact on flotation performance
A relatively inexpensive component may deserve priority if its failure repeatedly interrupts production. A more expensive component may be a better investment target if its service life can be extended significantly. The best ROI opportunity is therefore specific to each flotation circuit.
Before choosing a replacement, operators should identify the actual failure mechanism. Abrasive wear, impact damage, chemical degradation and mechanical problems may require different solutions. For a related diagnostic approach, see Hydrocyclone Underflow Too Wet? 6 Causes & Fixes.
Procurement Guide
A reliable ROI evaluation requires consistent data, a clear understanding of the failure mechanism and a fair comparison between alternatives.
Step 1: Identify the Existing Wear Problem
Review inspection records and determine whether the main issue is abrasive wear, impact, cracking, deformation, chemical degradation, installation problems or changes in rotor-stator clearance. Without identifying the failure mechanism, a replacement may repeat the same problem at a different purchase price.
Step 2: Confirm Material and Equipment Compatibility
Check the flotation machine model, component dimensions, mounting arrangement and required clearance. For rubber or polyurethane components, confirm the material’s suitability for the slurry chemistry, operating temperature and mechanical loading. For non-standard or OEM-compatible replacements, reviewing drawings before production helps reduce the risk of dimensional mismatches and installation delays.
Step 3: Compare Suppliers Beyond the Quotation
A technically capable supplier should be able to discuss material properties, dimensional requirements, manufacturing consistency and application conditions. Useful questions include:
What material formulation or grade is being proposed?
Can the production drawing be confirmed before manufacturing?
Is the component compatible with the existing flotation equipment?
What operating data is available to support the expected service life?
Can the supplier help investigate premature wear?
Step 4: Run a Controlled Trial
Where practical, test a replacement component under documented operating conditions. Record installation details, operating hours, tonnes processed, wear measurements, maintenance labor and relevant process indicators. Compare the results with the existing component under reasonably comparable conditions.
Step 5: Review Standardization Opportunities
Using compatible components across similar flotation cells can simplify purchasing, reduce inventory complexity and make maintenance planning easier. However, standardization should not override engineering requirements. Different cell models, rotor-stator geometries or operating conditions may require different replacement parts.
Step 6: Review Results Regularly
Update the cost calculation after each replacement cycle. Compare service hours, tonnes processed, replacement frequency, labor, downtime and process performance. If the results do not match expectations, investigate why before making a long-term purchasing decision.
Failure Analysis
| Problem | Possible Cause | Recommended Solution |
|---|---|---|
| Premature wear | Material mismatch or wrong grade | Verify slurry abrasiveness and select correct compound |
| Cracking | Impact loading or installation stress | Review mounting and consider rubber or composite |
| Deformation | Excessive temperature or chemical attack | Confirm material compatibility and operating limits |
| Poor fitment | Dimensional mismatch or drawing error | Confirm production drawing before manufacturing |
| Low efficiency | Rotor-stator clearance out of specification | Measure clearance and replace worn components |
| Excessive downtime | Frequent replacement or long lead time | Review supplier lead time and standardization |
| Installation failure | Incorrect torque or mounting procedure | Follow installation guide and inspect after start-up |
Maintenance Guide
Daily inspection: Check for unusual vibration, noise or power draw changes.
Weekly inspection: Review rotor-stator clearance and visible wear patterns.
Monthly inspection: Measure wear on rotors, stators, impellers and liners.
Wear pattern monitoring: Record wear location and rate to identify failure mechanism.
Replacement timing: Replace before geometry deteriorates beyond performance limits.
Spare parts inventory: Maintain critical spares based on actual consumption rate.
Downtime reduction: Plan replacements during scheduled shutdowns where possible.
Preventive maintenance: Use operating data to predict replacement intervals.
Case Study
Customer Type: Copper concentrator
Ore Type: Copper sulfide ore
Operating Conditions: Abrasive slurry, continuous operation, high tonnage
Problem: Flotation rotor and stator wear caused frequent shutdowns and unstable air dispersion.
Solution: Switched to a properly formulated polyurethane rotor and stator, confirmed dimensions before production, and implemented wear measurement records.
Result: Replacement interval extended by approximately 30%, maintenance labor reduced, and flotation stability improved. Actual results depend on site conditions and operating data.
Cost per Operating Hour Example
One of the simplest ways to compare alternative wear parts is to calculate their cost per operating hour.
Part cost + installation cost + attributable downtime cost / Operating hours
| Cost item | Option A | Option B |
|---|---|---|
| Purchase price | $600 | $900 |
| Installation cost per replacement | $100 | $100 |
| Service life | 3,000 | 6,000 |
| Cost per operating hour, excluding downtime | $0.233 | $0.167 |
In this example, Option B costs more initially but has a lower component-and-installation cost per operating hour. These figures are illustrative only. Actual ROI depends on real service life, maintenance requirements, downtime and operating performance.
Cost per Tonne Processed
For high-throughput plants, cost per tonne can be even more useful than cost per hour.
Relevant lifecycle costs / Tonnes processed during service life
This method allows maintenance teams to compare parts used under different production schedules, provided the data is sufficiently reliable and the operating conditions are comparable.
FAQ
Question: Why is the cheapest flotation wear part often the most expensive?
Answer: A cheap part that wears quickly may require more frequent replacements, additional labor and longer shutdowns. The total operating cost can exceed that of a more expensive part with a longer service life. Always compare cost per operating hour or tonne processed, not just purchase price.
Question: Which flotation wear parts have the biggest impact on operating costs?
Answer: Rotors and stators usually have the largest impact because they experience severe wear and directly affect flotation performance. Impellers, tank liners and wear plates can also be significant depending on the application. Review maintenance records to identify the highest-cost components in your circuit.
Question: Is polyurethane always better than rubber for flotation wear parts?
Answer: No. Polyurethane often performs well under continuous abrasion, while rubber offers better impact resistance. The right choice depends on slurry abrasiveness, particle size, impact loading, chemical exposure and equipment design. A controlled trial with wear measurements provides the strongest evidence.
Question: How do I calculate flotation wear part ROI?
Answer: Use cost per operating hour or cost per tonne processed. Include purchase price, installation cost and attributable downtime cost, then divide by operating hours or tonnes processed. Compare alternatives using the same cost categories for a fair evaluation.
Question: Can a longer-lasting rotor or stator still reduce ROI?
Answer: Yes. If the component adversely affects flotation performance or increases energy consumption, longer life alone does not guarantee better ROI. Mechanical durability and metallurgical performance should be assessed together.
Question: What information should I provide to a flotation wear part supplier?
Answer: Provide the flotation machine model, component dimensions, mounting arrangement, required clearance, slurry chemistry, operating temperature, particle size and wear history. Production drawings and OEM part numbers help reduce the risk of dimensional mismatches.
Question: How often should flotation wear parts be inspected?
Answer: Inspect daily for unusual vibration, noise or power draw changes. Check rotor-stator clearance weekly. Measure wear on rotors, stators, impellers and liners monthly. Record wear patterns to identify the failure mechanism and predict replacement intervals.
Question: Can flotation wear parts be standardized across multiple cells?
Answer: Standardization can simplify purchasing and reduce inventory complexity where cells are similar. However, different cell models, rotor-stator geometries or operating conditions may require different replacement parts. Standardize only where technically appropriate.
Question: What causes premature flotation rotor or stator wear?
Answer: Common causes include material mismatch, incorrect rotor-stator clearance, excessive impact loading, chemical attack and installation errors. Identifying the actual failure mechanism is essential before selecting a replacement.
Question: How does HUATAO support flotation wear part replacement projects?
Answer: HUATAO supplies polyurethane and rubber flotation rotors, stators, impellers and tank liners. Component selection can take into account slurry abrasiveness, particle size, solids concentration, chemical exposure, operating speed, rotor-stator clearance and wear pattern. Production drawings are available for customer confirmation before manufacturing.
Conclusion
The lowest-priced flotation wear part does not always deliver the best return on investment. Mining operators should compare cost per operating hour or tonne processed instead of relying only on the initial purchase price. Longer service life is valuable only when the flotation machine continues to perform as required. The best replacement strategy begins with the actual wear problem, correct material selection and verified installation. In short, the strongest ROI usually comes from matching the component to the application, maintaining correct geometry and installation, and using plant data to verify the result.
For mining plants seeking better ROI, the evaluation should focus on the total cost of ownership rather than material claims or purchase price alone. Explore related flotation components such as Flotation Spares (Rotor & Stator) and Flotation Impeller & Stator.
Related Products
Related Technical Guides
Flotation Cell Rotor and Stator Wear Parts: How They Control Recovery, Flow and Maintenance Cost
Rotor & Stator in Mechanical Flotation Cells: The Heart of Efficient Mineral Flotation
Hydrocyclone Wear: Root Causes, High-Wear Zones & Material Solutions
Improve Fine Screening Efficiency with Polyurethane Screen Panels
Related Buyer Guides
How Do I Choose the Right Rubber Belt for a Vacuum Belt Filter?
Which Manufacturer Offers High-Quality Polyurethane Tufflex Wire Screens for Mining?
Related Comparison Articles
Polyurethane Screen vs Rubber Screen vs Wire Mesh: A Complete Comparison Guide
Self-Cleaning Screen vs Traditional Woven Wire Mesh: Which One Should You Choose?
Annie Lu
Email: annie.lu@huataogroup.com
Phone / WhatsApp: +86 180 3242 2676
Website: http://www.tufflexscreen.com
#Flotation #MineralProcessing #WearParts #MiningMaintenance #ROI #Polyurethane #Rubber #RotorStator #FlotationCell #MiningEquipment #CostReduction #PlantAvailability #MaintenanceStrategy #HUATAO #TufflexScreen #FlotationRotor #FlotationStator #FlotationImpeller #TankLiner #WearPlate
admin