Is a Tufflex Screen Panel Better for Abrasive Screening?
-
 admin
- 03 Nov, 2026
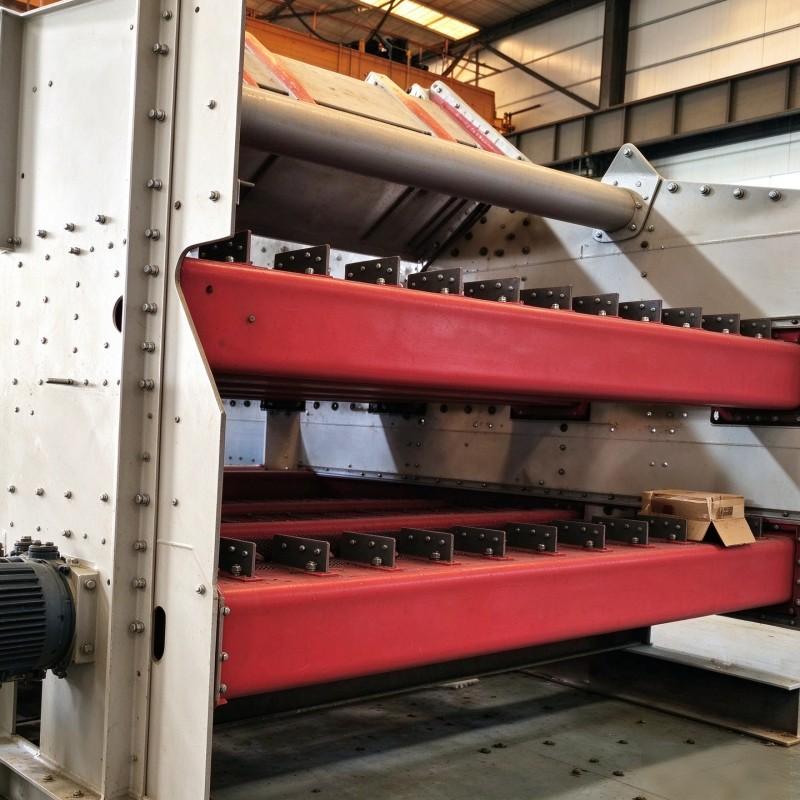
A Tufflex screen panel can be the better choice for abrasive screening when sliding abrasion is the dominant wear mechanism and the plant still needs an open screening structure. Polyurethane-coated wire rope provides a wear-resistant contact surface, while the rope-based cloth avoids the open-area penalty of a solid polyurethane panel. It is not automatically best for severe impact, very coarse feed or fine separation duty — those cases often favour rubber, heavy-duty polyurethane or a hybrid deck.
Key Takeaways
-
Abrasive screening is at least two problems. Sliding abrasion and concentrated impact pull media selection in opposite directions.
-
Tufflex targets sliding abrasion. The polyurethane coating provides the wear surface; the rope structure preserves open area.
-
Rubber still wins at the feed end. High-impact zones with large, heavy rock need energy absorption, not fine apertures.
-
Woven wire still wins on open area. Where abrasion is mild and capacity is the binding constraint, wire remains the economical choice.
-
Cost per tonne decides. Purchase price is not the metric; changeout frequency, downtime and throughput are.
Summary Table
| Item | Description |
|---|---|
| Function | Size separation at target cut with improved wear protection over woven wire |
| Material | Polyurethane-coated wire rope plus polyurethane-coated synthetic cord |
| Aperture | Square or rectangular, selected against target cut size and particle shape |
| Application | Abrasive ore, crushed rock, aggregates, hard minerals, wet or sticky feed |
| Service Life | Depends on abrasiveness, impact level, bed depth, tension and feed distribution |
| Benefits | Wear-resistant contact surface, open screening structure, configurable apertures |
Definition
Abrasive screening is the separation of hard, wear-causing material — mineral ore, crushed rock or aggregate — where the dominant cost driver is progressive surface wear of the screening medium rather than blockage or sizing accuracy alone.
Sliding abrasion occurs as particles travel across the deck and gradually remove material from the screening surface. Impact wear occurs where large particles land at the feed end and deliver concentrated local loads in a short time.
A Tufflex screen panel is a rope-based screening medium in which polyurethane-coated wire rope and polyurethane-coated synthetic cord are joined to form apertures. It sits between conventional WIRED & STEEL SCREEN MESH and solid POLYURETHANE & RUBBER SCREEN PANELS.
Working Principle
The panel works at three levels, and each one matters for abrasive duty.
Contact surface. The polyurethane coating around the wire rope is the surface that meets the feed. Polyurethane resists sliding abrasion well, so the contact area degrades more slowly than exposed metal wire in comparable duty. Coating thickness and formulation govern how much of that advantage is realised in practice.
Structural behaviour. Because the cloth is rope-based rather than a solid moulded panel, it retains flexibility. The cloth moves under vibration, which helps release lodged particles and reduces the tendency for fines to pack into apertures. Aperture geometry and welding configuration — fully versus partially welded — determine how much movement occurs.
Flow behaviour. In side-tensioned arrangements the synthetic cord runs parallel to the hooked edge and behaves similarly to rider bars, guiding oversize along the deck while fines migrate toward openings. This supports stratification and raises the proportion of feed that actually reaches an aperture.
Together these raise effective open area during operation. That is the figure that governs capacity — not the nominal open area on a product drawing. A panel with excellent nominal open area that blinds within an hour delivers less throughput than a modest panel that stays open.
Benefits
-
Longer service life than woven wire in sliding-abrasion duty, where wire wears out before it blinds.
-
More open area than solid polyurethane, because the rope structure leaves more of the deck available for material passage.
-
Flexible cloth behaviour that helps release lodged particles and reduces pegging pressure.
-
Configurable aperture geometry, allowing square or rectangular openings matched to the cut size.
-
Lower maintenance frequency, since fewer changeouts mean less labour and less planned downtime.
-
Measurable cost advantage when evaluated as cost per tonne processed rather than price per panel.
None of these benefits is unconditional. In severe impact zones, or where feed is exceptionally coarse, other media remain better suited to the duty. Stating otherwise would be marketing, not engineering.
Applications
Tufflex is evaluated where abrasive wear, not blockage alone, is the maintenance driver.
-
Gold ore and alluvial feed with hard, angular particles and variable moisture.
-
Iron ore and copper ore scalping and sizing ahead of GRINDING, where wire wear is frequent.
-
Aggregates and crushed rock production, where hard limestone or granite shortens wire life.
-
Silica sand duty where both abrasion and fine sizing matter.
-
Coal preparation where clay partings and abrasive shale occur together.
-
Lead zinc ore and nickel ore in mixed wet and abrasive duty.
-
Tailings and slurry duty where abrasive solids and moisture combine.
The panel typically sits between size reduction in CRUSHING and downstream CLASSIFICATION. Wear-driven screen failures there propagate as unstable feed sizing into the grinding and classification circuit, which is why a screen change can show up as a mill performance issue weeks later.
Material Comparison
| Property | Tufflex | Woven Wire Mesh | Solid Polyurethane Panel | Rubber Screen Media |
|---|---|---|---|---|
| Sliding abrasion resistance | Good | Moderate | Good–excellent | Good |
| Impact resistance | Moderate | Low | Moderate | Excellent |
| Open area | Good | High | Lower | Moderate |
| Anti-pegging | Good (flexible cloth) | Poor on near-size | Moderate | Moderate |
| Noise | Low | High | Low | Low |
| Best application | Abrasive duty with open-area needs | Clean dry high-capacity duty | Wet screening, high wear | Coarse high-impact feed zones |
The table is a starting point, not a verdict. Woven wire remains correct where abrasion is mild and capacity dominates. Rubber remains correct where impact dominates. Tufflex earns its place where sliding abrasion is the cost driver but solid polyurethane would sacrifice too much open area.
Application Comparison
| Scenario | Dominant Problem | Recommended Direction |
|---|---|---|
| Hard angular ore, wire wears out fast | Sliding abrasion | Tufflex with aperture matched to cut size |
| Large rock at high drop height | Impact | Rubber at feed end, Tufflex downstream |
| Mild abrasion, capacity constrained | Open area | Woven wire or hybrid deck |
| Wet sticky feed with clay | Blinding | Polyurethane surface plus moisture control |
| Fine cut with tight tolerance | Sizing accuracy | POLYURETHANE FINE SCREEN PANEL |
| Mixed wear and pegging | Both | Tufflex trial with separate wear benchmarking |
Industry Application Matrix
| Industry | Typical Ore | Wear Risk | Screening Stage |
|---|---|---|---|
| Gold | Gold ore, alluvial | High abrasion | Pre-concentration, GOLD PROCESS EQUIPMENT feed prep |
| Iron ore | Iron ore, hematite | High abrasion | Scalping and product sizing |
| Copper | Copper ore | High abrasion | SAG discharge screening |
| Coal | Coal with shale partings | Moderate | Desliming and preparation |
| Aggregates | Limestone, granite | High abrasion | Product classification |
| Industrial minerals | Silica sand | Moderate–high | Fine screening and dewatering |
| Battery minerals | Lithium ore | Moderate | Classification feed prep |
| Base metals | Lead zinc ore, nickel ore | High | Grinding circuit screening |
| Fertilizer | Phosphate ore | Moderate | Wet screening |
| Critical minerals | Rare earth ore | Moderate | Fine classification |
Selection Guide
1. Identify the wear mechanism. Inspect worn panels. Even surface loss across the deck indicates sliding abrasion. Concentrated damage at the feed end indicates impact. The two need different answers, and a single panel may not solve both.
2. Confirm the cut size and aperture. Match aperture dimensions and shape to the target separation and the near-size fraction. Where pegging coexists with wear, test a rectangular aperture. A material change cannot compensate for a fundamentally wrong opening.
3. Check the deck compatibility. Verify panel dimensions, hook profile, support spacing and tensioning direction. Many “premature wear” complaints are actually fitment problems. Review the SCREENING ACCESSORIES before blaming the panel.
4. Consider a hybrid layout. A BANANA SCREEN deck with a thin, well-distributed bed often benefits from rubber at the impact zone and Tufflex or fine polyurethane downstream. This is usually cheaper than optimising one media for two conflicting duties.
5. Baseline before you buy. Record panel life, changeout hours, unplanned downtime, throughput and product size distribution on the VIBRATING SCREENS deck. Without a baseline, no trial result is credible.
Procurement Guide
Required information: feed material and abrasiveness, maximum feed size and size distribution, target cut size, current aperture dimensions, moisture and clay content, current media type and wear pattern, deck dimensions, support arrangement, tensioning direction, hook configuration, and screen machine operating data.
Drawings needed: panel outline with tolerances, hook profile, aperture pattern and pitch, rope and cord layout, and any cut-outs or reinforcement details.
OEM part numbers: obtain original panel references where available and confirm whether the supplier supports direct OEM replacement.
Material selection: confirm the polyurethane formulation and hardness, and request material reports rather than relying on datasheet claims.
MOQ, lead time, packaging and shipping: confirm trial-quantity MOQ, lead time against your shutdown window, packaging suitable for long panels, and shipping method.
Inspection standards: dimensional check against drawing, aperture measurement, hardness verification, and visual inspection of coating integrity and weld quality.
Supplier evaluation checklist — ask directly:
-
Can you manufacture according to our drawings?
-
Can you provide material reports?
-
Can you support OEM replacement?
-
Do you have export experience in our region?
-
Can you provide wear-life recommendations for our ore?
A supplier who answers all five with documentation is a different risk profile from one who answers with a catalogue. The WHICH MANUFACTURER OFFERS HIGH-QUALITY POLYURETHANE TUFFLEX WIRE SCREENS FOR MINING? guide expands on these questions.
Failure Analysis
| Problem | Possible Cause | Recommended Solution |
|---|---|---|
| Premature wear | Abrasive ore, unsuitable PU grade, excessive bed depth | Review material grade; reduce bed depth; re-baseline wear life |
| Cracking | Impact from oversize, incorrect tension, damaged support bars | Inspect supports; correct tension; add impact protection |
| Blinding | High clay or moisture, fines buildup | Review moisture control, aperture size, feed distribution |
| Pegging | Near-size particles, square aperture | Test rectangular aperture; review weld configuration |
| Low efficiency | Uneven feed, wrong aperture, incorrect inclination | Check LINEAR VIBRATING FEEDER spread; verify settings |
| Excessive downtime | Frequent cleaning, poor panel fitment | Log cleaning events by location; verify hook and tension fit |
| Poor fitment | Incorrect panel dimensions or hook profile | Re-measure against drawing; confirm hook configuration |
| Material mismatch | PU grade unsuited to the ore | Request formulation review and material report |
| Installation damage | Incorrect tensioning, worn supports | Retrain crew; inspect accessories |
Maintenance Guide
Daily: visual check for wear progression, loose edges and material buildup. Record where wear occurs, not only how much.
Weekly: inspect tension and clamping; check edge wear and coating damage; confirm feed spreads across the full deck width.
Monthly: measure remaining thickness at known high-wear zones; review the changeout log; verify support bars and screen motion.
Wear pattern monitoring: photograph high-wear zones at fixed intervals so comparisons remain valid over time.
Replacement timing: plan on measured wear rate rather than on failure. Hold a rolling spare-panel inventory sized to your shutdown cycle.
Downtime reduction: pre-stage panels and accessories before shutdown and standardise panel dimensions across decks where possible.
Preventive maintenance: treat feed distribution and bed depth as maintenance items. In practice they shorten panel life more than most media defects.
Case Study
Customer Type: Mid-size aggregates operation producing crushed granite.
Ore Type: Hard, angular granite with high silica content.
Operating Conditions: Two-deck inclined screen, woven wire media, feed drop height approximately one metre at the feed end.
Problem: Wire mesh worn through within six to eight weeks on the upper deck; frequent changeouts; measurable unplanned downtime; product sizing drifting as apertures wore open.
Solution: Trial of polyurethane-coated Tufflex panels on the upper deck, with rubber impact media retained at the feed zone. Aperture matched to the target cut size, and feed distribution corrected to reduce bed depth at the centre of the deck.
Result: Panel life extended to roughly three times the wire baseline in the trial section; changeout frequency reduced by about 60 percent; more stable product sizing because apertures no longer wore open. The wear rate did not change on the impact zone, which confirmed rubber was the correct choice there.
Figures reflect a realistic single-site trial and are not a guaranteed performance claim.
FAQ
Q1: Is Tufflex suitable for abrasive mining materials?
It can be suitable for selected abrasive duties because polyurethane-coated wire rope provides a wear-resistant contact surface while the rope structure maintains open area. Suitability depends on the material, impact level, aperture, coating design and operating conditions. Confirm the configuration for the specific application rather than assuming a general fit.
Q2: Does Tufflex last longer than woven wire mesh?
It may provide longer service life in suitable sliding-abrasion applications, but the improvement is not universal. A meaningful comparison requires operating data from the same material, feed conditions and screening duty. In severe impact zones, wire and Tufflex may both fail quickly while rubber survives.
Q3: Is Tufflex better than a solid polyurethane screen panel?
Not in every situation. Tufflex has a rope-based composite structure; solid polyurethane is a moulded panel. Tufflex generally offers more open area, while solid panels can offer higher wear volume in severe abrasion. Compare open area, wear requirements, aperture options and impact conditions before deciding.
Q4: Can Tufflex handle high-impact screening?
That depends on feed size, drop height, impact concentration and panel design. For very high-impact feed zones, evaluate heavy-duty polyurethane, rubber or localized impact protection. Many plants combine rubber at the feed end with Tufflex downstream, which addresses both mechanisms without over-specifying one media.
Q5: How do I choose the correct Tufflex aperture?
Start with target separation size, feed size distribution, particle shape and required throughput. Then confirm aperture dimensions and construction with the supplier. The largest feed particle alone is not enough to determine the correct aperture, and near-size content often matters more for pegging risk.
Q6: How much do Tufflex screen panels cost?
Price depends on panel size, aperture pattern, rope and cord construction, welding configuration, polyurethane grade and quantity. Trial quantities are usually quoted separately from production volume. Evaluate against cost per tonne processed over a full campaign, including changeout labour and downtime, rather than against purchase price per panel.
Q7: Can Tufflex panels replace woven wire directly?
Not universally. Panel dimensions, hook profile, tensioning direction, support layout and aperture geometry must all be confirmed. Treat any replacement as an engineered fit rather than a drop-in swap. Fitment errors are a common cause of premature failure that is wrongly attributed to the material.
Q8: Does reduced pegging mean longer wear life?
No. These are separate outcomes. A panel may reduce pegging without lasting longer in abrasive duty, and a wear-resistant panel may still blind under unsuitable moisture conditions. Track wear life and blockage frequency as independent indicators so procurement decisions rest on the right evidence.
Q9: How do I know whether my problem is wear or impact?
Inspect the failed panels. Even surface loss across the deck indicates sliding abrasion. Concentrated damage at the feed end, often with cracking or deformation, indicates impact. Many plants have both, at different points on the same deck, and a hybrid layout is often the most economical answer.
Q10: How should I run a trial?
Select one representative deck section, record baseline panel life, changeout hours, downtime, throughput and product sizing, then install the trial media and monitor the same indicators over a comparable period. Where possible, keep feed conditions consistent and document any changes so the comparison remains valid.
Conclusion
Tufflex screen panels are worth evaluating for abrasive screening applications that need polyurethane surface protection and a rope-based screening structure. They may provide a useful balance between wear protection and screening performance, but the result depends on the selected design and the material being processed.
Before a full-deck change, assess abrasion, impact, aperture requirements, open area, installation compatibility and current maintenance costs. Where the feed end receives heavy impact, retain rubber or heavy-duty protection in that zone and use Tufflex downstream. Where possible, conduct a controlled trial and compare service life, throughput, screening efficiency and cost per tonne.
If your operation is replacing screens too frequently or losing throughput to wear-related downtime, HUATAO can review your application requirements and identify a suitable Tufflex configuration for evaluation.
Related Articles
Related Products
Related Technical Guides
-
IMPROVE FINE SCREENING EFFICIENCY WITH POLYURETHANE SCREEN PANELS
-
HYDROCYCLONE WEAR: ROOT CAUSES, HIGH-WEAR ZONES & MATERIAL SOLUTIONS
-
FLOTATION CELL ROTOR AND STATOR WEAR PARTS: HOW THEY CONTROL RECOVERY, FLOW AND MAINTENANCE COST
-
ROTOR & STATOR IN MECHANICAL FLOTATION CELLS: THE HEART OF EFFICIENT MINERAL FLOTATION
Related Buyer Guides
-
WHICH MANUFACTURER OFFERS HIGH-QUALITY POLYURETHANE TUFFLEX WIRE SCREENS FOR MINING?
-
HOW DO I CHOOSE THE RIGHT RUBBER BELT FOR A VACUUM BELT FILTER?
Related Comparison Articles
-
POLYURETHANE SCREEN VS RUBBER SCREEN VS WIRE MESH: A COMPLETE COMPARISON GUIDE
-
SELF-CLEANING SCREEN VS TRADITIONAL WOVEN WIRE MESH: WHICH ONE SHOULD YOU CHOOSE?
Contact
Annie Lu
Email: annie.lu@huataogroup.com
Mobile / WhatsApp / WeChat: +86 18032422676
Website: https://www.tufflexscreen.com
#Tufflex #AbrasiveScreening #PolyurethaneScreen #ScreenMedia #MiningScreening #Aggregates #MineralProcessing
Tags:
 admin
personal profile