Which Screen Media Survives Wet Coal Screening?
Nov 2, 2026
 admin
Quick Answer: A belt tracking system keeps a wandering conveyor belt centered using the belt’s own motion as the steering input. It is worth the investment whenever drift is causing edge wear, spillage, seized return rollers, or unplanned stops. Mechanical trackers need no power and cost less than one replacement belt; automatic trackers hold a tighter band on long or heavily loaded conveyors. They correct symptoms, so feeding, tension, and cleaning still have to be right.
What Is a Conveyor Belt Tracking System?
A tracking system is hardware fitted to the conveyor structure that steers the belt back toward center when it starts to run off-line. The passive type uses a pivoting frame with angled rollers; the belt pushes against the rollers and the frame responds. The automatic type adds a sensing arm and continuous powered or hydraulic correction. Both types live on the return side, the carrying side, or both, depending on where the drift happens.
Engineers sometimes group trackers with Belt Conveyors accessories as a minor item. On a mine site, treating tracking as minor is how belts end up replaced years early.
Key Takeaways
✔ A tracker converts belt drift into a steering correction automatically, with no operator in the loop on most designs.
✔ The payback comes from belt edge life, cleanup labor, return roller survival, and avoided splice failures.
✔ Underload drift points at feed distribution; constant drift points at structure, tension, or the belt itself.
✔ Trackers correct locally. Long conveyors need staged units or a continuous automatic correction.
Summary Table
| Item | Description |
| Function | Holds the belt centered on idlers and pulleys without manual adjustment |
| Material | Welded steel frame, PU-coated or rubber steering rollers, sealed pivots |
| Application | Return side, carrying side, staged positions on overland runs |
| Service Life | Frame outlives several belts; rollers and pivot bearings serviced annually |
| Benefits | Longer belt life, less spillage labor, fewer unplanned stoppages |
Definition
In conveyor engineering, tracking describes the belt’s lateral position as it travels. Good tracking means the belt runs centered within its structure; mistracking means one or both edges move toward the frame. A tracking system is the machinery that corrects that lateral position continuously. It complements the Conveyor Belts themselves and the idler sets that support them, and it works alongside the cleaners, skirting, and loading equipment that determine how much material ends up where it shouldn’t be.

Conveyor profile diagram showing idler positions, take-up, and pulley arrangement along a belt line
Conveyor geometry from the side. Tracker positions sit clear of the take-up and drive pulley, where tension makes correction unpredictable.
Working Principle
The rule that makes every tracker work is this: a belt moves toward whichever side of a roller it contacts first. Tension, crowning, and idler squareness determine where that first contact happens. Change the angle of the roller near the belt edge and you change the steering force.
A passive tracker exploits the rule directly. Its steering rollers sit on a pivoting frame, often with two rollers angled in opposite directions. When the belt edge drifts toward one side, it climbs the angled roller, and the resulting lateral force walks the belt back toward center. There’s no sensor and no power supply. The belt’s own misbehavior is the control signal. This is why mechanical trackers are so reliable in the field: the failure modes are mechanical and visible, a stiff pivot or a stopped roller, and an inspector’s hand can find both in a minute. The Belt Tracker family covers the common layouts.
An automatic tracker closes the loop differently. A sensing arm rides near the belt edge; when the edge moves out of the set band, hydraulic or motorized adjustment re-angles a tracking idler continuously. The band it holds is much tighter than a passive unit can manage, and it reacts in seconds instead of over tens of meters of belt travel. That matters on long or high-tension conveyors, where a passive frame would correct the wrong direction for a minute or more before the correction arrives. Purpose-built units like the Conveyor Belt Tracker are dimensioned for belt class and width, which is why the specification matters at purchase.
Two limits apply to both types. First, a tracker corrects locally; a unit at position 50 m cannot steer position 300 m. Second, the tracker assumes a sane running line. Worn Conveyor Idlers & Rollers, a bent stringer, or a pulley that has lost its lagging will defeat any tracker, and the wear parts will pay for it.
Benefits
Belt life improves first, because the edge damage mechanism stops. A belt edge rubbing structure loses cover every single revolution; at 2 m/s, that’s 170 km of rubbing per day. Cleanup labor drops next, since material stops falling off the drifting edge along the stringers. Return rollers live longer because spilled fines stop packing around their ends. Splices last because a centered belt loads them evenly. And the operational benefit compounds quietly: the belt stops being the thing everybody watches during the shift. For a maintenance planner, a tracker converts a variable, human-dependent task into a fixed, mechanical one, and that conversion is where most of the value sits.
Applications
Any drifting conveyor is a candidate, but the economics are clearest in four places: long overland runs, where drift develops faster than a walk-round can catch it; loading zones after crushers, where lumps and uneven feed knock the belt sideways; wet or sticky duties, where material buildup changes the tracking from hour to hour; and reversing conveyors, which drift in both directions by nature. The whole Conveyor section of a mine benefits once tracking stops being a recurring manual job.
Material Comparison
Roller material decides how the tracker ages in your environment.
| Steering roller material | Behavior in dry duty | Behavior in wet/sticky duty | Wear pattern |
| Plain steel | Good | Material packs, roller stalls | Even shell wear |
| PU-coated | Good | Better; buildup sheds | Coating wears first |
| Rubber disc | Good | Self-cleaning between discs | Disc edge wear |
| Sealed unit + PU | Best service life | Best overall | Bearing outlasts coating |
Frames follow the environment: painted carbon steel indoors, galvanized or heavier coating outdoors and in corrosive sites. Pivot bearings deserve the same attention; sealed units cost little more and remove a greasing task from the round.
Application Comparison
A short in-plant belt, clean duty, occasional drift: one passive unit on the return side solves it, and that’s the cheapest fix in conveying. A long overland belt: passive units staged every 100 meters or so, or one automatic tracker doing what the staged units cannot. A high-tension belt: confirm frame rating, because a loaded belt pushing an edge can overwhelm a light frame. A reversing shuttle belt: only a bidirectional design makes sense, otherwise every return stroke undoes the correction. A belt that drifts only under load: a carrying-side tracker helps, but the honest answer is that the chute is the problem, and the Guide Trough and liner condition should be reviewed before any tracker is ordered.
Industry Application Matrix
| Industry | Where tracking pays first | Dominant mechanism |
| Coal | Washery feed and product belts | Wet fines, buildup, spillage |
| Iron ore | Overland and stockyard belts | Abrasive lumps, edge wear |
| Copper | Concentrator feed conveyors | High tonnage, heavy loading |
| Gold | Remote overland runs | Low staffing, long correction delays |
| Aggregates | Portable and stacker conveyors | Frequent moves, realignment labor |
Selection Guide
Start with the drift signature. Track the belt empty and loaded, in dry and wet conditions if both exist on site. Empty-only drift points at tension or the belt itself. Loaded-only drift points at feed distribution. Constant drift in one direction points at structure or pulley geometry. Each signature leads to a different tracker choice and a different position.
Then collect the numbers: belt width and class, cover thicknesses, speed, tonnage, conveyor length and profile, pulley diameters, take-up type. With those, supplier sizing is a desk exercise. The Belt Tracker selection notes cover most mining configurations, and a supplier who asks for photos of the drift condition is worth engaging further.
Procurement Guide
Field engineers usually inherit the procurement conversation late. If you get a say, ask four things. What are the wear parts, and what do they cost in year two? Can the supplier build to OEM drawings for future lines? What’s the lead time on a roller set, packed for export? And will they put a wear-life recommendation in writing? The Which Manufacturer Offers High-Quality Polyurethane Tufflex Wire Screens for Mining? buyer guide makes the same point for screen media, and it holds here: the supplier’s willingness to commit to numbers before the order is the best predictor of what the support looks like after it.
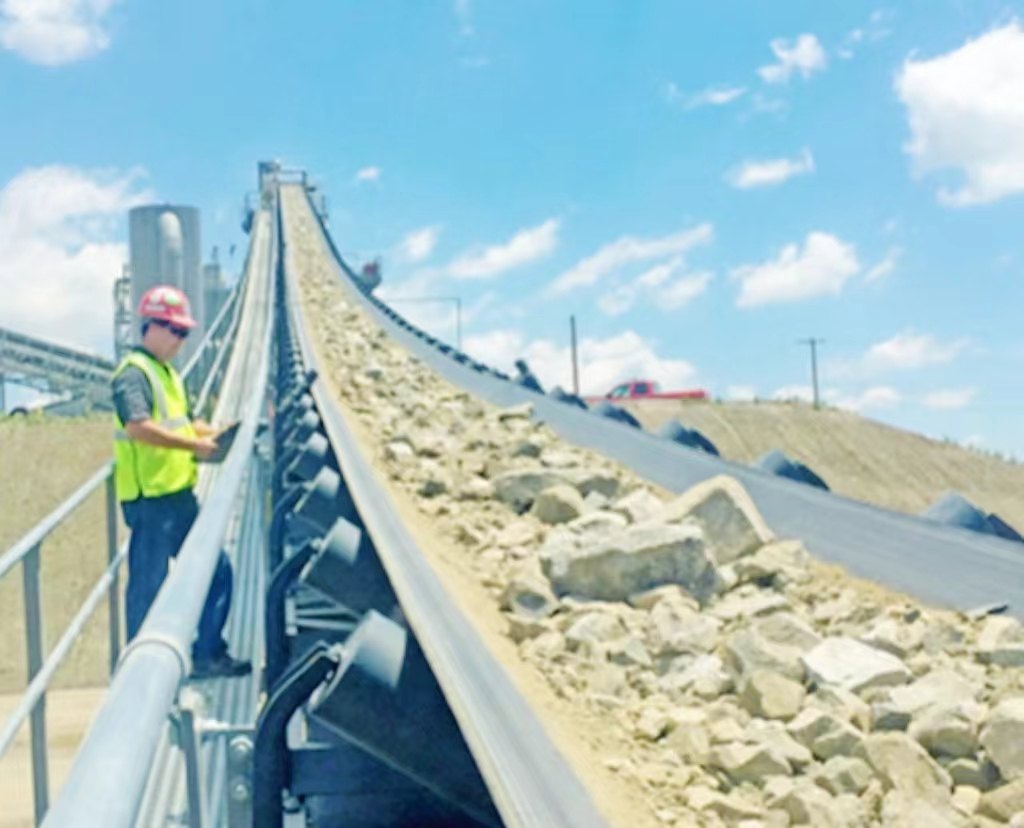
Technician in a high-visibility vest inspecting the idlers along a long elevated conveyor
Most tracker failures announce themselves on the inspection walk, weeks before they reach production.
Failure Analysis
| Problem | Possible cause | Recommended solution |
| Premature roller wear | Abrasive dust ingress at bearing | Sealed units, dust caps, shelter |
| Tracker stops correcting | Pivot frozen by packed material | Clear buildup, sealed pivot, inspection cadence |
| Correction too slow | Rollers glazed or worn small | Replace rollers at measured wear limit |
| Belt oscillates | Tracker too close to pulley | Reposition to design distance |
| Corrects wrong way | Reversing belt with one-way design | Fit bidirectional tracker |
| Frame cracked at weld | Undersized for belt tension | Re-rate frame, confirm belt class |
| Drift returns every wet season | Feed pattern changes with moisture | Review chute, Conveyor Belt Skirting and feed arrangement |
That last row is the one field engineers meet most. The tracker gets blamed in the wet season; the material pattern changed and the tracker is absorbing a change it was never sized for.
Maintenance Guide
The rhythm is light. Monthly: check pivot play, confirm every roller turns, look for material packed around the frame, and watch the belt through one full loaded pass. After any spill or wash-down: clear the frame before material sets. Yearly: measure roller wear at a marked point, replace on trend, grease anything not sealed, and re-verify frame squareness with a straight edge. Cleaning hardware is part of the tracking system in practice; a primary blade and a Mining Secondary Belt Cleaner that actually work keep carryback off the return rollers and off the crowned pulleys, and Polyurethane Conveyor Belt Cleaner Blades hold their edge long enough for that protection to be real rather than theoretical. The same logic applies to the Conveyor Belt Cleaner / Scraper range as a whole: clean pulleys keep their crown, and crowned pulleys are half of what makes a belt track.
Case Study
Customer Type: Iron ore mine, overland conveying
Ore Type: Hematite, crushed and screened
Operating Conditions: 420 m overland conveyor, 1,400 mm belt, high tension, dust exposure
Problem: Belt edge wear and repeated splice alarms; drift worse after rain; fitters re-centering the belt weekly by adjustment
Solution: Automatic tracker near the head pulley, passive unit near the tail, idler audit along the worst 100 m, cleaning overhaul at the head
Result: Belt held within a stable band through the wet season, splice alarms stopped, the weekly adjustment task moved to the monthly inspection round
FAQ
Q: How does a passive tracker steer without power?
A: Its steering rollers sit at opposing angles on a pivoting frame. When the belt edge drifts into one roller, the contact angle generates a lateral force that walks the belt back toward center. The belt’s own movement is the control signal, so the unit needs no sensor, no supply, and no operator input.
Q: Why does my belt track fine empty but drift loaded?
A: Loading changes everything. Off-center feed pushes the belt sideways, and the added weight changes the tension profile. A carrying-side tracker manages the symptom, but the durable fix is upstream: check the chute, the liner wear, and the feed arrangement. Fix the pattern and the tracker stops working overtime.
Q: How close to a pulley should a tracker sit?
A: Typically within 15 to 20 meters of the head or tail pulley, and never immediately adjacent. Too close and the belt’s tension profile makes the correction unpredictable; oscillation is the usual symptom. The design distance depends on belt class and speed, which is why position belongs in the supplier’s scope.
Q: What wears out first on a tracking system?
A: The steering rollers and pivot bearings. Rollers wear small and lose their steering angle; pivots stiffen when material packs around them. Both are visible on a monthly walk-round long before they affect the belt. Frames rarely wear out; they get damaged by events.
Q: Can one tracker control a whole conveyor?
A: No. Correction is local. A unit at position 50 meters cannot steer position 300 meters, and on long runs the drift at the far end develops before any correction arrives. Stage passive units along the run or use an automatic tracker for continuous control. Spacing beats quantity every time.
Q: Does a tracker help with spillage?
A: Indirectly but strongly. Most stringer spillage comes off a drifting edge. Hold the belt centered and the spill source disappears, which cuts cleanup labor and stops fines packing around return rollers. It’s one of the few upgrades that removes labor instead of adding it.
Q: What information does a supplier need to size a tracker?
A: Belt width and class, cover thicknesses, speed, tonnage range, conveyor length and profile, pulley diameters, take-up type, and the intended mounting position. Photos of the drift condition help more than expected. With that set, sizing and quantity confirmation is a desk exercise.
Q: Are automatic trackers worth the premium?
A: On long, high-tension, or reversing conveyors, yes: the band they hold is tighter and their reaction is faster than any staged passive layout. On short, clean, low-tension belts, a passive unit does the job for a fraction of the cost. The decision variable is how far and how fast the drift develops.
Conclusion
A belt tracking system is a mechanical answer to a mechanical problem, and that’s why it works. It reads the belt’s own motion, steers it back, and does so every revolution without asking anyone for help. Size it from the drift signature, place it near the pulleys, keep it clean, and keep the cleaning and feeding systems honest around it. Do those four things and the investment question answers itself in the first belt life.
Related Articles
Related Products
Related Technical Guides
Related Buyer Guides
Related Comparison Articles
Contact
Annie Lu
Email: annie.lu@huataogroup.com
WhatsApp/WeChat: +86 18032422676
Website: www.tufflexscreen.com
admin