For recovering fine particles (typically 0.075 to 1 mm), high-frequency vibrating screens generally offer superior fines recovery and separation efficiency compared to hydrocyclones.
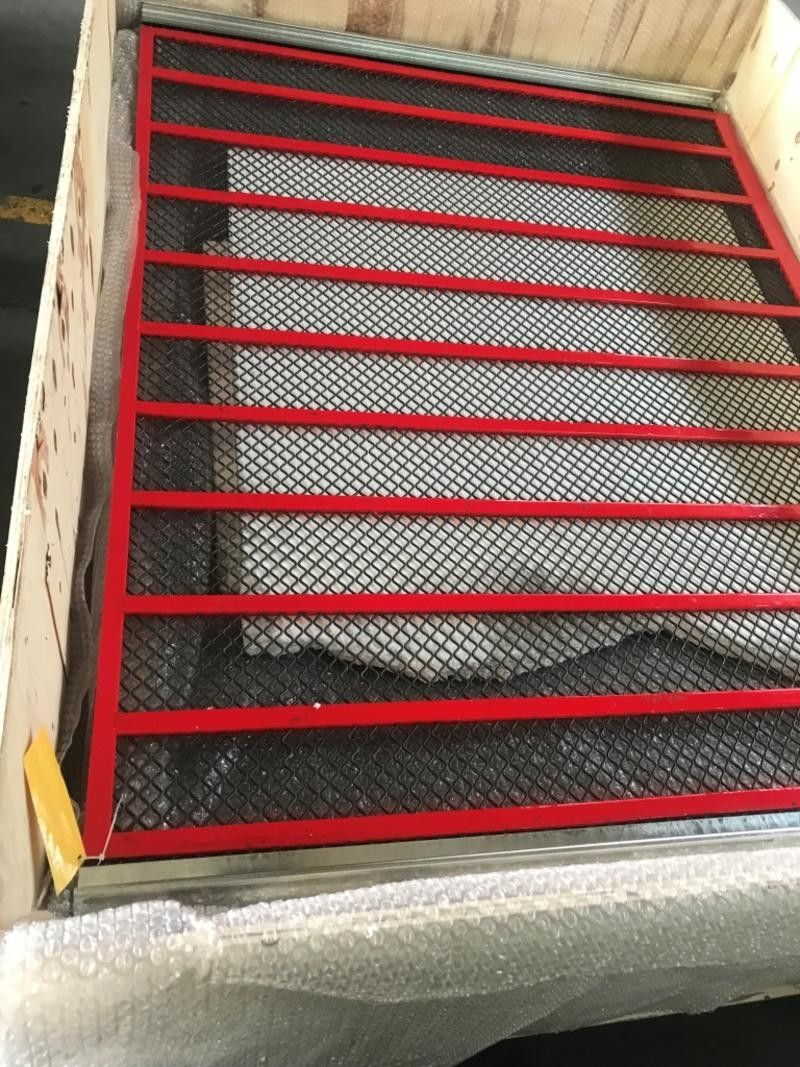
Mongolian Mining Corporation operates as a medium-sized coal washing enterprise, with an annual raw coal processing capacity of 15 million tons. Its production process combines heavy medium cyclones and flotation technology. However, the plant faced significant challenges in two key stages—final coal dehydration and coal slime classification—due to its original stainless steel screens:
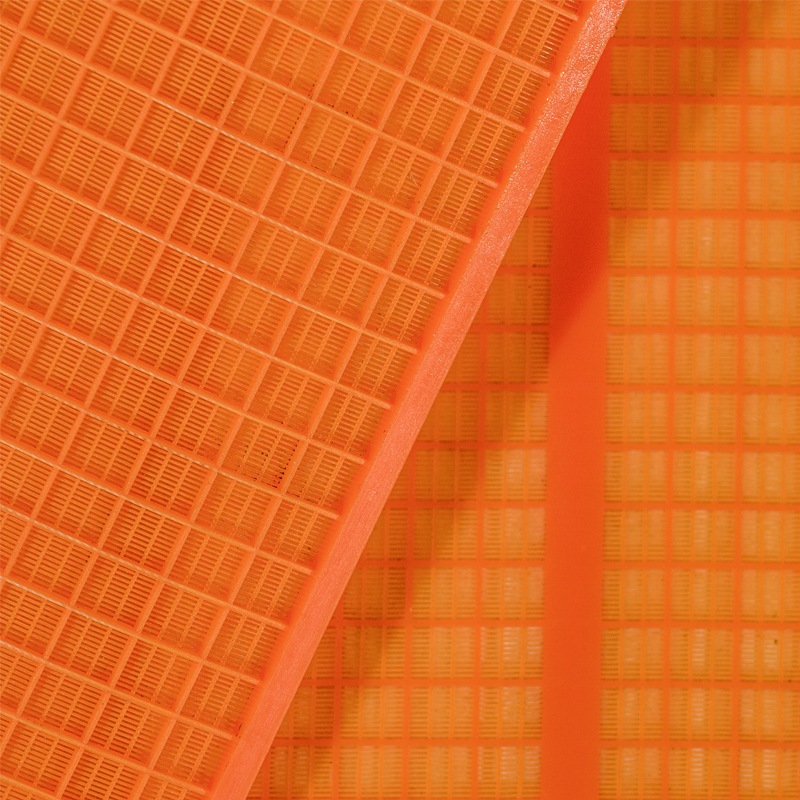
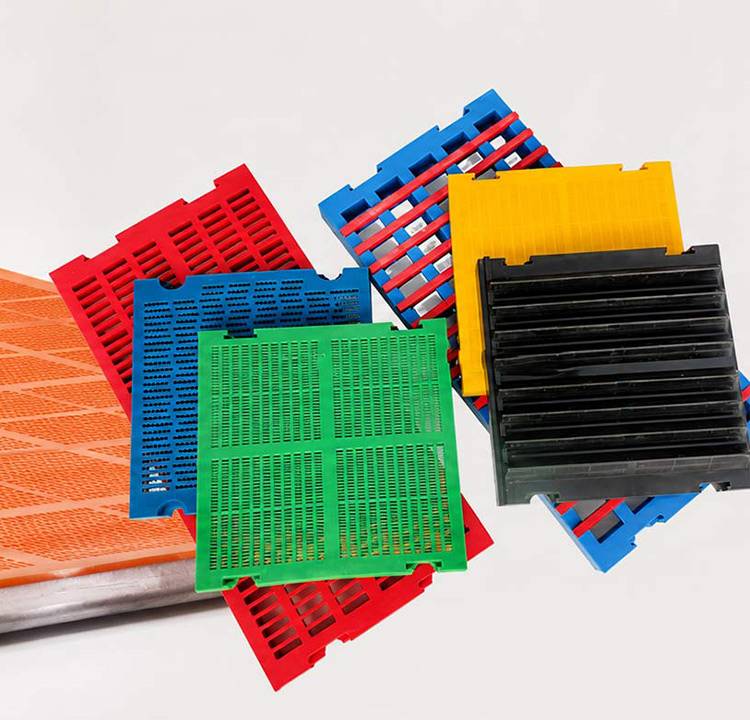
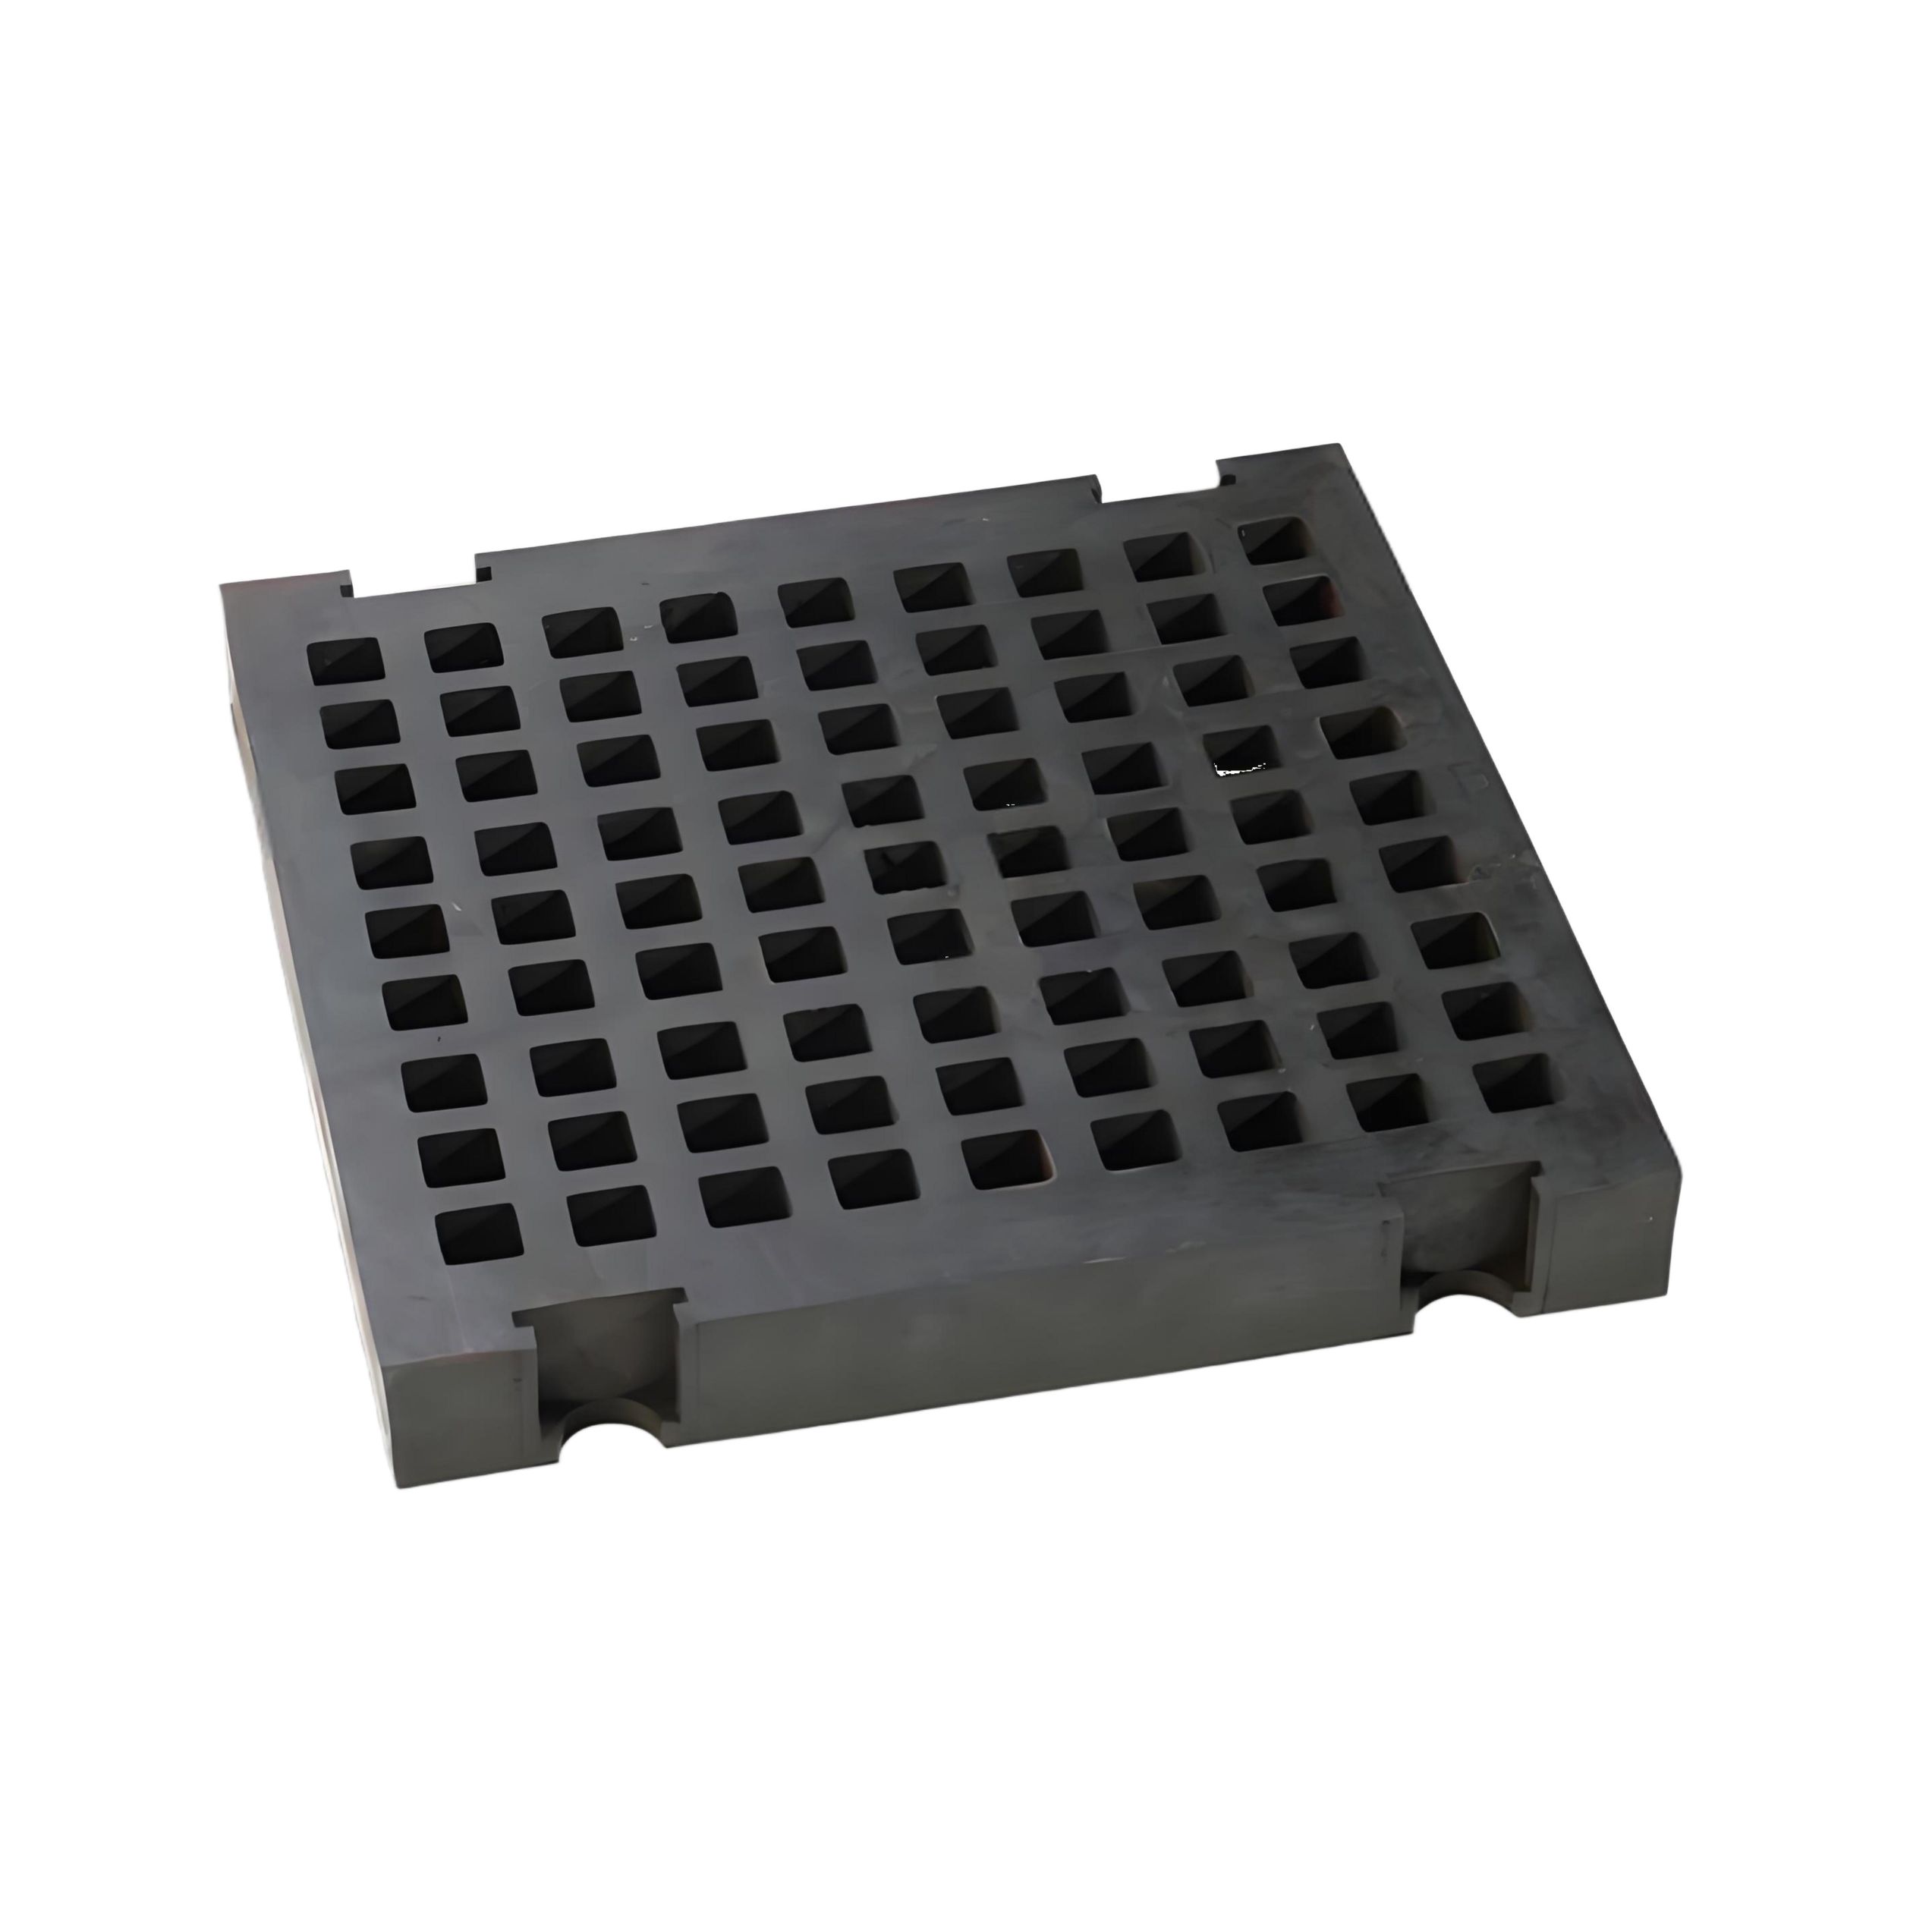
Polyurethane screen panels offer superior wear resistance (8–10× better than steel), longer service life (2–4× longer), excellent anti-blinding performance for wet and sticky materials, lower noise levels (5–15 dB reduction), easier maintenance with modular systems, and stable screening accuracy. While initial cost is higher, polyurethane screens deliver lower total cost of ownership through reduced replacement frequency, minimized downtime, and improved screening efficiency in challenging mining applications.
As mining and aggregate operations demand higher efficiency and finer material classification, traditional screening solutions are no longer sufficient.
A building materials manufacturer based in Minas Gerais, Brazil, grappled with severe screen clogging caused by wet aggregates—exacerbated by the region’s annual rainfall of over 1,800 mm. Prior attempts to fix the issue with two common screen types failed miserably:
In the dry screening processes of mining operations, traditional metal screen plates often fall short—they wear out rapidly, tear easily, and get clogged frequently. These issues lead to reduced production efficiency and skyrocketing maintenance costs.