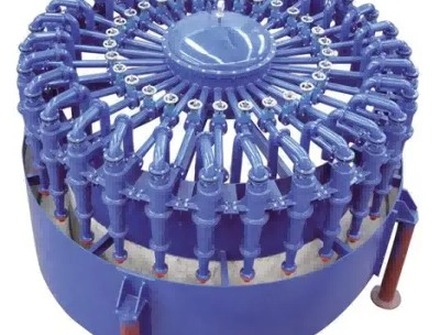
How Do I Properly Inspect Hydrocyclone Wear Parts?
-
 admin
- 21 Oct, 2026
How Do I Properly Inspect Hydrocyclone Wear Parts?
Quick Answer
Inspecting hydrocyclone wear parts is a structured process of measurement and observation, not just a visual walk-by. Focus on three primary wear points: (1) Spigot/apex—measure internal diameter with a bore gauge; replace when enlarged by 3–5 mm or 7–20%. (2) Vortex finder—inspect every 3–6 months; replace when wear exceeds 2 mm. (3) Cone liner—use ultrasonic thickness gauge; replace when wall thickness drops by 50% or cracking appears. Daily visual checks of underflow pattern, leaks, and feed pressure catch early warning signs.
Key Takeaways
✔ Spigot/apex — measure internal diameter with bore gauge; replace at 3–5 mm or 7–20% enlargement
✔ Vortex finder — inspect every 3–6 months; replace when wear exceeds 2 mm
✔ Cone liner — use ultrasonic thickness gauge; replace at 50% wall thickness loss
✔ Underflow pattern — umbrella spray = normal; roping = spigot too small; too wide = spigot worn
✔ Log the numbers — trend wear rate; predict replacement
✔ Compare within a cluster — one cyclone behaving differently = compromised wear parts
✔ Safety first — isolate, depressurize, drain before internal inspection
Summary Table
| Component | How to Inspect | Replacement Trigger |
|---|---|---|
| Spigot / Apex | Bore gauge or caliper | Enlarges by 3–5 mm or 7–20% |
| Vortex Finder | Measure ID; check wall thinning | Wear exceeds 2 mm |
| Cone Liner | Ultrasonic thickness gauge (UT) | 50% wall thickness loss or cracking |
Definition
What Is Hydrocyclone Wear Part Inspection?
Hydrocyclone wear part inspection is the systematic measurement and observation of critical internal components—spigot, vortex finder, and cone liner—to detect wear before separation efficiency degrades.
What Is Condition-Based Maintenance?
Condition-based maintenance means replacing components based on measured wear rather than a fixed calendar schedule. For hydrocyclones, this involves regular measurement of critical dimensions and trending the results over time.
Working Principle
How Wear Affects Performance
-
Spigot Wear: Enlarges opening → underflow becomes dilute → fine particles misreport
-
Vortex Finder Wear: Increases short-circuit flow → coarse particles report to overflow
-
Cone Liner Wear: Changes internal geometry → separation sharpness declines
-
Performance Loss: Overflow coarsens; recovery drops
-
Replacement: Restore geometry before efficiency is compromised
Benefits
Benefits of Structured Inspection
-
Predictable maintenance — schedule based on data
-
Optimal performance — maintain separation efficiency
-
Reduced downtime — replace before failure
-
Lower cost per ton — avoid premature or reactive replacement
-
Stable operation — consistent classification
-
Extended component life — no unnecessary changes
Applications
Hydrocyclone Applications Where Inspection Matters
-
Gold recovery — abrasive quartz
-
Copper ore processing — high tonnage
-
Iron ore processing — very abrasive
-
Coal preparation — moderate abrasion
-
Tailings management — high wear
-
FGD gypsum — chemical and abrasive
Material Comparison
Wear Part Material Options
| Material | Wear Resistance | Cost | Best Application |
|---|---|---|---|
| Silicon Carbide | Excellent | High | Extreme abrasion |
| Alumina Ceramic | Very Good | Moderate-High | High-abrasion zones |
| Polyurethane | Good | Moderate | Moderate abrasion |
| Rubber | Moderate | Low | Impact areas |
Application Comparison
Wear Rate by Component
| Component | Wear Rate | Inspection Frequency |
|---|---|---|
| Spigot (Apex) | Fastest | Weekly measurement |
| Vortex Finder | Second | Every 3–6 months |
| Lower Cone | Moderate | Quarterly |
| Upper Cone | Slow | Annually |
Industry Application Matrix
| Industry | Typical Inspection Challenge | Primary Solution |
|---|---|---|
| Gold Ore | Abrasive quartz | Weekly spigot measurement |
| Copper Ore | High tonnage | Quarterly vortex finder inspection |
| Iron Ore | Very abrasive | UT measurement of cone liner |
| Coal | Moderate abrasion | Visual checks; periodic measurement |
| Tailings | High wear | Condition-based replacement |
| FGD Gypsum | Chemical and abrasive | Ceramic components |
Selection Guide
Step-by-Step Inspection Routine
Step 1: Daily Visual Checks
-
Observe underflow pattern
-
Check for leaks and vibrations
-
Log feed pressure
Step 2: Weekly Spigot Measurement
-
Use bore gauge or caliper
-
Record internal diameter
-
Replace at 3–5 mm or 7–20% enlargement
Step 3: Quarterly Vortex Finder Inspection
-
Measure internal diameter
-
Check for wall thinning
-
Replace when wear exceeds 2 mm
Step 4: Annual Cone Liner Inspection
-
Use ultrasonic thickness gauge
-
Check for cracking or tearing
-
Replace at 50% wall thickness loss
Step 5: Log and Trend
-
Record all measurements against asset ID
-
Trend wear rate
-
Predict replacement needs
Step 6: Compare Within Cluster
-
Identify cyclones behaving differently
-
Investigate compromised wear parts
Procurement Guide
Key Considerations When Procuring Hydrocyclone Wear Parts
Required Information:
-
Hydrocyclone model and size
-
OEM part numbers (spigot, vortex finder, cone liner)
-
Current wear rates and replacement frequency
-
Feed conditions (pressure, density, PSD)
-
Ore type and abrasiveness
Supplier Evaluation Checklist:
-
□ Does the supplier offer multiple material options?
-
□ Can they provide wear-life guarantees?
-
□ Do they offer ceramic or high-chrome options?
-
□ What is the typical lead time?
-
□ Can they provide dimension verification?
Buyer Questions to Ask:
-
“What material do you recommend for my spigot?”
-
“Can you provide a wear-life comparison for ceramic vs rubber?”
-
“Do you offer a trial program for wear parts?”
-
“What is the recommended inspection schedule?”
Failure Analysis
| Problem | Possible Cause | Recommended Solution |
|---|---|---|
| Rapid spigot wear | Abrasive ore | Upgrade to ceramic |
| Vortex finder wear | High velocity | Replace at 2 mm wear |
| Cone liner cracking | Impact damage | Check for tramp material |
| Uneven wear | Poor feed distribution | Check feed box |
| Overflow coarsening | Worn vortex finder | Replace vortex finder |
| Dilute underflow | Worn spigot | Replace spigot |
| High maintenance cost | Reactive replacement | Implement condition-based maintenance |
Maintenance Guide
Recommended Inspection Schedule
| Frequency | Task |
|---|---|
| Daily | Observe underflow pattern; check for leaks; log pressure |
| Weekly | Measure spigot diameter |
| Monthly | Check for tramp material; inspect feed |
| Quarterly | Measure vortex finder; full internal inspection |
| Annually | UT measurement of cone liner; complete overhaul |
Preventive Maintenance Tips
-
Log the numbers, don’t eyeball — trend wear rate
-
Compare within a cluster — one behaving differently = compromised
-
Safety first — isolate, depressurize, drain
-
Keep spare parts — avoid downtime
-
Consider standby cyclone — eliminate mill shutdowns
Case Study
Case Study: Implementing Structured Inspection at a Copper Mine
Customer Type: Large copper mine
Ore Type: Copper porphyry, moderate abrasion
Operating Conditions: 6-cyclone cluster, 200 tph feed
Problem:
The mine was experiencing unplanned downtime due to hydrocyclone wear. Spigots were failing without warning, causing overflow to run coarse and reducing flotation recovery by 5%. Maintenance was reactive.
Solution:
A structured inspection routine was implemented:
-
Weekly spigot measurement with bore gauge
-
Quarterly vortex finder inspection
-
Annual UT measurement of cone liners
-
Logging all measurements against asset ID
-
Comparing within cluster to identify anomalies
Result:
-
Unplanned downtime reduced by 80%
-
Flotation recovery improved by 4%
-
Spigot life extended from 4 weeks to 8 weeks (2× longer)
-
Annual savings from reduced downtime and improved recovery: $1.6 million
-
Investment payback period: less than 2 months
FAQ
Question 1: What is the most critical measurement for hydrocyclone inspection?
Answer: The spigot/apex internal diameter. Use a bore gauge or caliper. Replace when the bore enlarges by 3–5 mm or exceeds 7–20% of the original size. This is the fastest-wearing component and directly affects underflow density and separation efficiency.
Question 2: How often should I inspect the vortex finder?
Answer: Every 3–6 months. The vortex finder is buried inside the top of the cyclone and is often overlooked. Measure the internal diameter and check for wall thinning. Replace when wear exceeds 2 mm.
Question 3: What is the replacement trigger for cone liners?
Answer: Replace when wall thickness drops by 50% or when cracking/tearing appears. Use an ultrasonic thickness gauge (UT) to measure wall thickness, especially in the lower cone where wear is heaviest.
Question 4: What does the underflow pattern tell me?
Answer: A normal discharge is a hollow, umbrella-shaped spray. Roping indicates the spigot is too small or feed is too dense. A spray that is too wide and dilute suggests the spigot has worn too large. This is your real-time diagnostic.
Question 5: Why is logging measurements important?
Answer: Logging actual measurements against the cyclone’s asset ID lets you trend wear rate and predict when the next replacement is due. This is condition-based maintenance rather than reactive replacement.
Question 6: How do I compare performance within a cluster?
Answer: In a cluster fed from a common header, if one cyclone is behaving differently from its neighbors—different underflow pattern, different pressure drop—it is a strong sign that its internal wear parts are compromised. Investigate that cyclone first.
Question 7: What safety precautions should I take before internal inspection?
Answer: Always isolate the cyclone, depressurize, and drain it before doing internal inspections or removing parts. Follow lockout/tagout procedures and wear appropriate PPE.
Question 8: What is the practical inspection schedule?
Answer: The schedule: (1) Daily visual checks of underflow pattern, leaks, and pressure. (2) Weekly spigot measurement. (3) Quarterly vortex finder inspection. (4) Annual UT measurement of cone liner. (5) Log all measurements and trend wear.
Conclusion
Inspecting hydrocyclone wear parts is a structured process of measurement and observation. Focus on three primary wear points: spigot/apex, vortex finder, and cone liner.
Key Takeaways:
-
Spigot/apex — measure internal diameter with bore gauge; replace at 3–5 mm or 7–20% enlargement
-
Vortex finder — inspect every 3–6 months; replace when wear exceeds 2 mm
-
Cone liner — use ultrasonic thickness gauge; replace at 50% wall thickness loss
-
Underflow pattern — umbrella spray = normal; roping = spigot too small; too wide = spigot worn
-
Log the numbers — trend wear rate; predict replacement
-
Compare within a cluster — one cyclone behaving differently = compromised wear parts
-
Safety first — isolate, depressurize, drain before internal inspection
Establish a routine where you measure critical dimensions and log results to trend wear over time. This lets you predict replacement needs rather than react to failures.
Related Articles
Related Products:
Related Technical Guides:
Related Process Hubs:
Related Category Hubs:
Contact Us
We warmly welcome customers from around the world to contact us and establish mutually beneficial partnerships.
Contact: Annie Lu
Email: annie.lu@huataogroup.com
Phone / WhatsApp: +86 180 3242 2676
Website: https://www.tufflexscreen.com/
Tags: Hydrocyclone, Wear Parts, Inspection, Maintenance, Spigot, Vortex Finder, Cone Liner, Mineral Processing, Condition-Based Maintenance, Hydrocyclone Optimization
Tags:
 admin
personal profile