-
 admin
- 20 Nov, 2026
Quick Answer
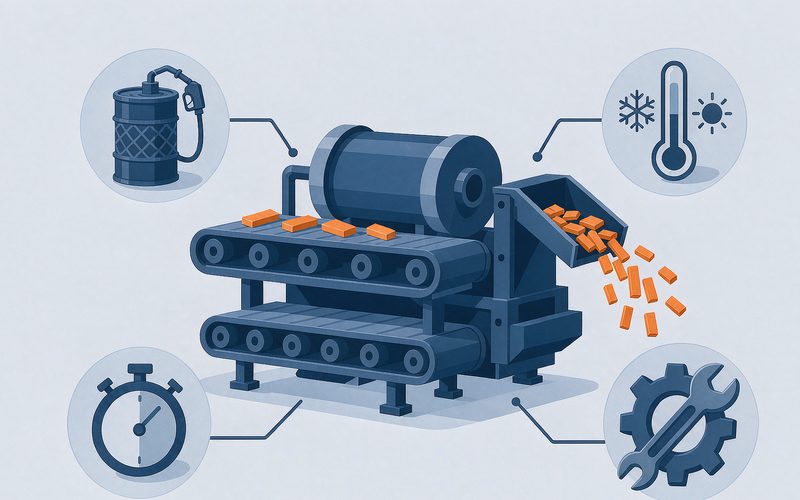
For most track-mounted and wheeled mobile crushing plants, the best power choice for a self-cleaning iron remover follows one simple rule: if the plant already carries a diesel generator large enough for the crusher and conveyors, power the magnet electrically from that genset — ideally with a permanent-magnet block and only the cleaning belt drawing power (0.75–2.2 kW), which adds almost no fuel burn. If the plant has no genset at all (hydraulic-only machines such as compact track impactors), drive the magnet’s cleaning belt with a dedicated hydraulic motor fed through a priority flow valve from the host pump circuit — cheaper to install and simpler to maintain, but expect ±10% belt-speed drift with oil temperature, and never use the hydraulic option for an electromagnetic coil. Choose the genset route for long campaigns, hot material, fine tramp iron, or sites where discharge reliability is critical; choose the hydraulic route for short-rental demolition and recycling work where the plant moves daily and simplicity wins. Either way, a self-cleaning magnet typically pays for itself within one crusher downtime event it prevents.
Key Takeaways
- The power debate concerns the cleaning belt drive and coil supply— a permanent magnetic field itself consumes nothing.
- An electromagnetic self-cleaning magnet adds a steady 3–9 kW coil load; on genset-fed plants this can push the generator one size class up and raise fuel burn by 1.5–2.0 L/h.
- Hydraulic belt drives are cheaper to fit but suffer belt-speed drift of ±10% with oil temperature and pump wear; discharge geometry assumes a fixed speed.
- Below –20 °C, engine-driven hydraulics tolerate cold better than standard electric motors and gensets.
- Demolition and recycling contractors (short rental cycles) lean hydraulic; quarry and mining campaign sites lean genset-electric.

FAQ
Q1: Can I power a self-cleaning electromagnetic iron remover from a hydraulic circuit?
No. The electromagnetic coil needs rectified DC at high amperage; hydraulics can drive only the cleaning belt. If the magnet is electromagnetic, a genset is mandatory.
Q2: How much extra fuel does a self-cleaning magnet really burn on a mobile plant?
A permanent-magnet unit with an electric belt adds roughly 0.2–0.4 L/h; an electromagnetic unit adds 1.5–2.0 L/h because the coil runs continuously; a hydraulic belt drive adds about 0.3–0.6 L/h through engine load.
Q3: Will a hydraulic-driven magnet belt slow down as the machine warms up?
Yes, by up to ±10% across oil-temperature extremes, depending on valve design. Since the discharge trajectory depends on belt speed, drift can push captured iron back onto the conveyor. A priority flow valve and a speed sensor substantially reduce this risk.
Q4: Can I connect the magnet to the plant’s generator without resizing it?
Only if the continuous load at 80% genset capacity still leaves room for the coil plus belt starting surge. The practical rule is to reserve an additional 10–15 kVA when adding an electromagnetic self-cleaning magnet.
Q5: Is a permanent magnet strong enough for crusher protection?
For coarse tramp iron — demolition steel, rebar, teeth, plate — a properly sized permanent overband magnet captures reliably. For fine or deeply buried steel under heavy burden, an electromagnetic deep-field unit remains the technical benchmark.
Q6: What happens to the magnet in freezing weather?
Below –20 °C, standard gensets and electric belt motors lose start reliability and torque. Either specify cold-start packages (block heater, battery warmer, arctic fuel) or choose a hydraulic belt drive with arctic-grade oil.
Q7: Should the magnet run while the crusher is paused?
Yes, ideally. Tramp iron accumulates on a stopped conveyor and hits hardest at restart. On diesel-electric plants, feed the magnet belt from a small auxiliary outlet so cleaning continues during pauses.
Q8: Why does my hydraulic magnet discharge iron short of the chute in the morning but fine in the afternoon?
Cold oil. Belt speed is lowest at morning start-up and rises with oil temperature — the trajectory moves. Re-aim the chute for the cold condition and fit a speed-compensated valve.
Q9: Can one magnet protect both the primary and secondary crusher on a mobile train?
Usually not. Place one magnet ahead of each crusher, or ahead of the single most vulnerable machine. A magnet protecting an Impact Crusher does not protect a downstream cone from steel that entered after the magnet.
Q10: What documentation should I demand from the supplier?
Coil kW and inrush data, belt-speed trajectory charts at ±10% speed, vibration-hardening specifications for electrical components, commissioning test records at three feed rates, and a spares list with lead times from the Magnetic Separation Spares channel.
Conclusion
 Conclusion
The diesel-generator-versus-hydraulic question for a self-cleaning iron remover is not a matter of brand loyalty — it is a load-accounting and duty-cycle problem. Electromagnetic magnets require genset power, full stop, with a 10–15 kVA reserve. Permanent-magnet units split cleanly: genset-electric powering wins wherever a generator already exists, thanks to stable belt speed and marginal fuel cost near zero; hydraulic powering wins on hydraulic-only rental machines running coarse tramp iron over short campaigns, provided the circuit uses a priority valve and the chute geometry tolerates drift. Cold climates, remote fuel logistics, and deep-burden ore work each push the decision in predictable directions — and the framework above turns those pushes into a seven-step selection process. HUATAO supplies self-cleaning electromagnetic separators, permanent-magnet overband units, magnetic drums and rollers, conveyor protection components, and crusher wear parts for mobile and fixed plants worldwide, and engineers the magnet, chute, and power interface as one system rather than a box on a bracket.
Related Articles
- Self-Cleaning Electromagnetic Separator
- Electromagnetic Overband Separator
- Magnetic Separators
- Magnetic Drums & Rollers
- Iron Magnet
- Vibrating Screens
- Crushing
- Products
- Conveyor
- Contact Us
Contact Us
Contact: Annie Lu
Email: annie.lu@huataogroup.com
Phone / WhatsApp: +86 180 3242 2676
Website: http://www.tufflexscreen.com
We warmly welcome custo
 admin
personal profile
No prev page
Previous Post