Why Is My Self-Cleaning Magnet Discharging Iron Into the Wrong Chute After a Belt Replacement?
-
 admin
- 20 Nov, 2026
Quick Answer
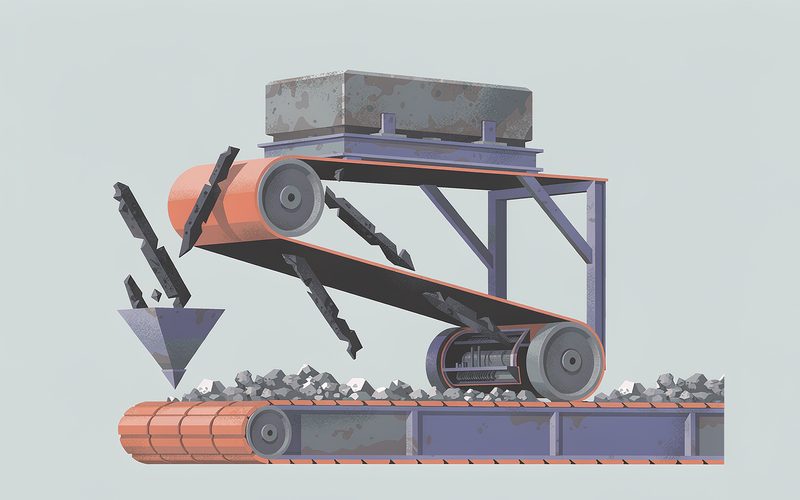
Your self-cleaning magnet did not change — the conveyor around it did. A new belt is usually thicker and stiffer than the worn one it replaced, which raises the belt surface closer to the magnet face, changes the take-up position, and alters the iron release point. Because the discharge trajectory of captured tramp iron depends on belt surface height, cleat position, belt speed and the geometry of the discharge pulley and chute lip, even a 15–25 mm change in belt top height can throw iron past the chute opening and into the product chute, the tail chute, or onto the ground. Fixing it is a geometry problem: measure the new gap, re-check the chute lip position against the actual release point, and re-commission with a marked landing grid before returning to full production.
Case Study: One Belt Replacement, One Shift to Fix
Customer Type: Iron ore processing plant, 1,600 mm trunk conveyor feeding secondary crushing
Ore Type: Magnetite iron ore, high tramp iron incidence from mining front
Operating Conditions: 1.8 m/s belt speed, 2,000 t/h, bed depth ~180 mm, cross-belt electromagnetic separator over the head section
Problem: After the annual belt replacement (fabric belt upgraded from 4-ply to 5-ply), captured tramp iron began arcing over the reject chute lip and landing in the product transfer chute. Within two days, operators recovered steel fragments from the SAG mill feed belt; one near-miss with a pump impeller forced a 6-hour unplanned stoppage.
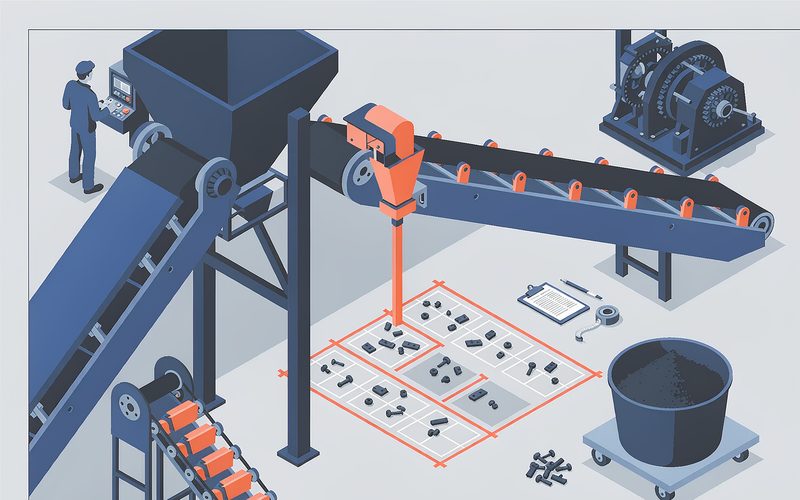
Solution: A landing grid test showed the release point had rotated forward by approximately 45 mm due to the thicker belt closing the magnet gap from 320 mm to 288 mm and the fresh high-friction cover holding iron longer around the discharge roller. The crew re-shimmed the magnet frame to restore a 300 mm gap, moved the chute lip 60 mm forward on new slotted brackets, and reset the splitter plate that had been re-hung 30 mm off position during the belt work.
Result: Follow-up grid test captured 96% of test pieces in the reject chute (from 61% before correction); zero steel recovered from downstream equipment over the following 90 days; total correction time 3.5 hours, of which 2 hours were production-free. The plant now runs the landing grid test at every belt change as standard practice.
FAQ
Q1: Why did the magnet only start mis-discharging after the belt was replaced?
A: The magnet’s release point is geometry-dependent. The new belt’s thickness, stiffness and surface friction moved the release point 20–60 mm, which was enough to carry iron past the chute lip. The magnet itself never changed; the conveyor geometry did.
Q2: How much can a new belt realistically shift the iron landing point?
A: Field experience shows 20–60 mm from thickness and friction changes alone, and 100 mm or more if belt speed also changed. A landing grid test measures the actual shift in your plant rather than estimating it.
Q3: Can I just move the chute instead of adjusting the magnet?
A: Yes, if the capture rate is still acceptable. Moving the chute lip under the new trajectory is often faster. But if the gap changed by more than 20 mm, correct the gap too — capture performance and trajectory are linked through the same geometry.
Related Articles
Related Products
- Self-Cleaning Electromagnetic Separator
- Electromagnetic Overband Separator
- Magnetic Drum
- Magnetic Roller
- Iron Magnet
Related Technical Guides
- Improve Fine Screening Efficiency with Polyurethane Screen Panels
- Self-Cleaning Screen vs Traditional Woven Wire Mesh: Which One Should You Choose?
- Polyurethane Screen vs Rubber Screen vs Wire Mesh: A Complete Comparison Guide
- Which Manufacturer Offers High-Quality Polyurethane Tufflex Wire Screens for Mining?
- How Do I Choose the Right Rubber Belt for a Vacuum Belt Filter?
Related Buyer Guides & Categories
- Crusher Wear Parts
- Conveyor Idlers & Rollers
- Conveyor Belt Tracker
- Heavy-Duty Conveyor Impact Bed
- Conveyor Belt Skirting
- Mining Secondary Belt Cleaner
- HUATAO Mining Screen
Contact Us
Contact: Annie Lu
Email: annie.lu@huataogroup.com
Phone / WhatsApp: +86 180 3242 2676
Website: http://www.tufflexscreen.com
We warmly welcome customers from around the world to contact us and establish mutually beneficial partnerships.
 admin
personal profile
No prev page
Previous Post